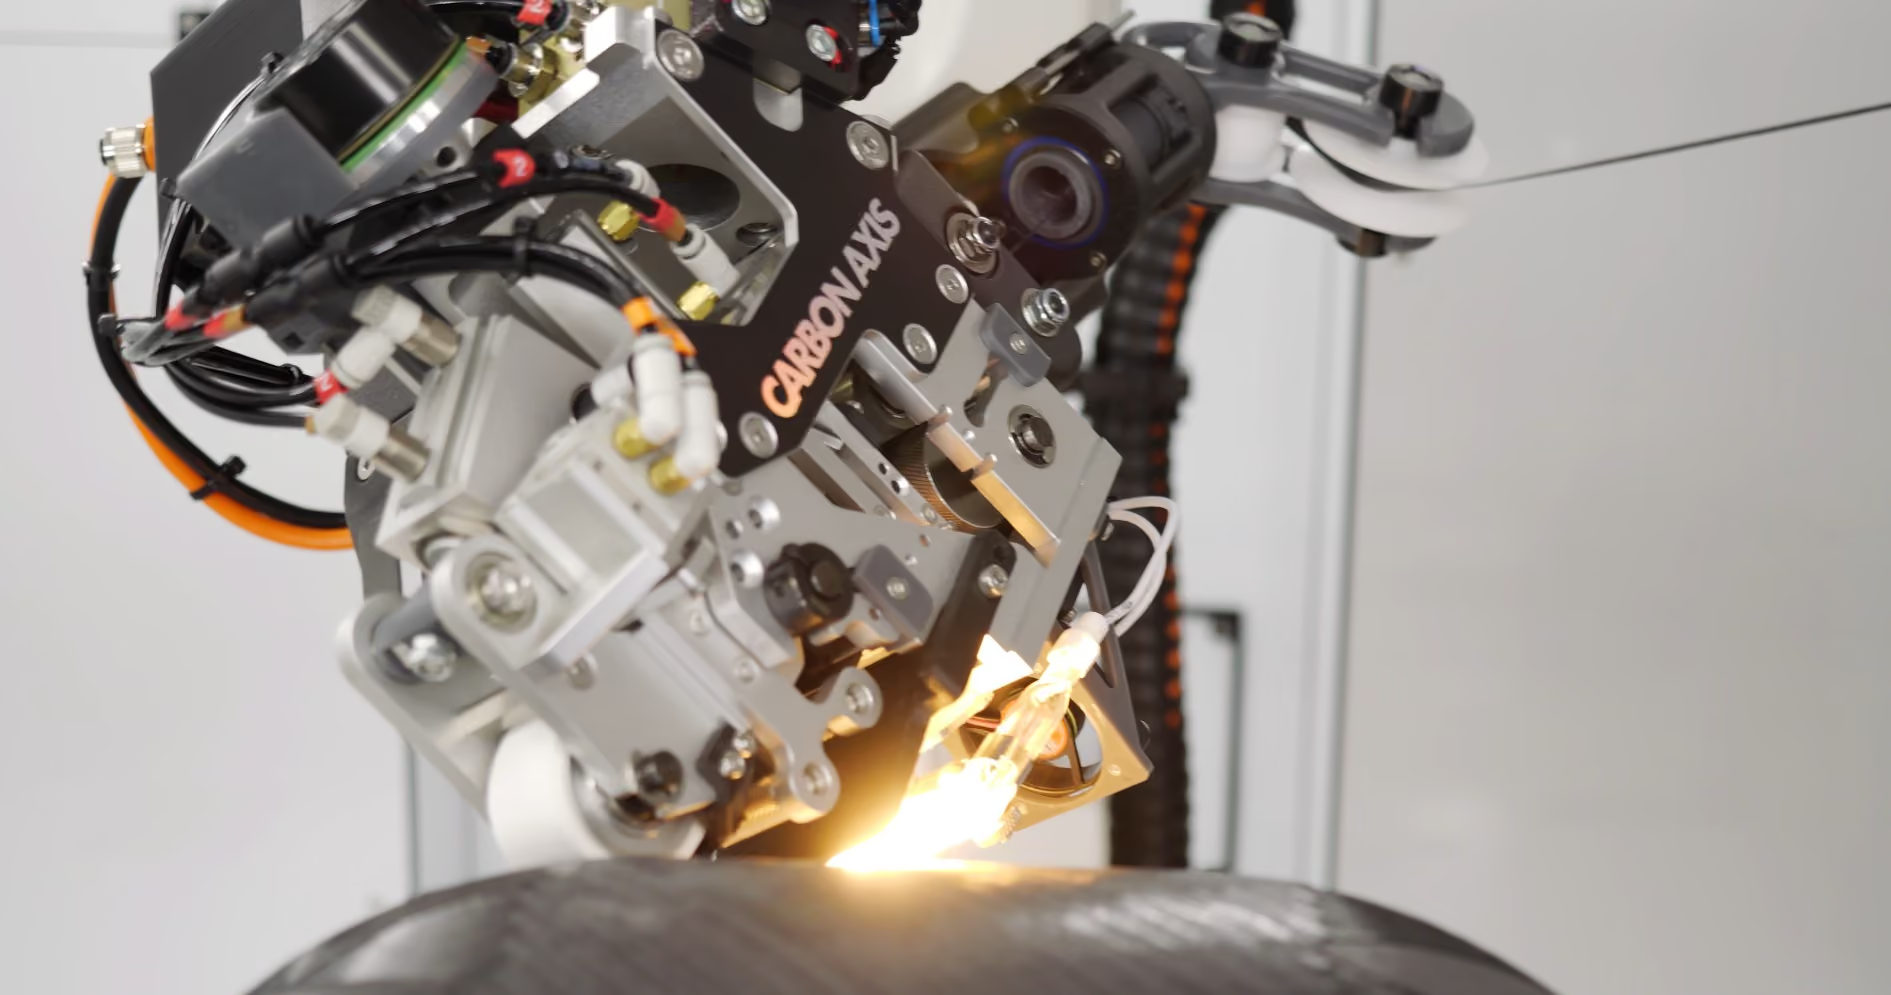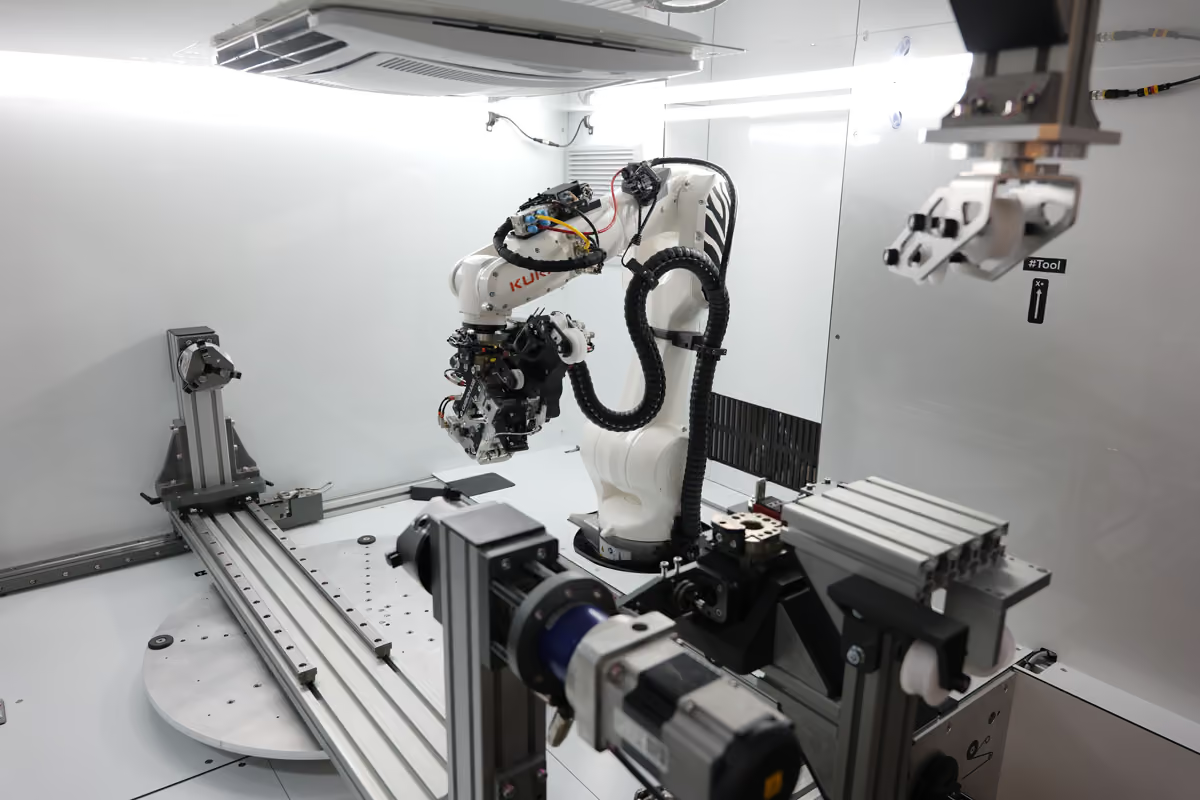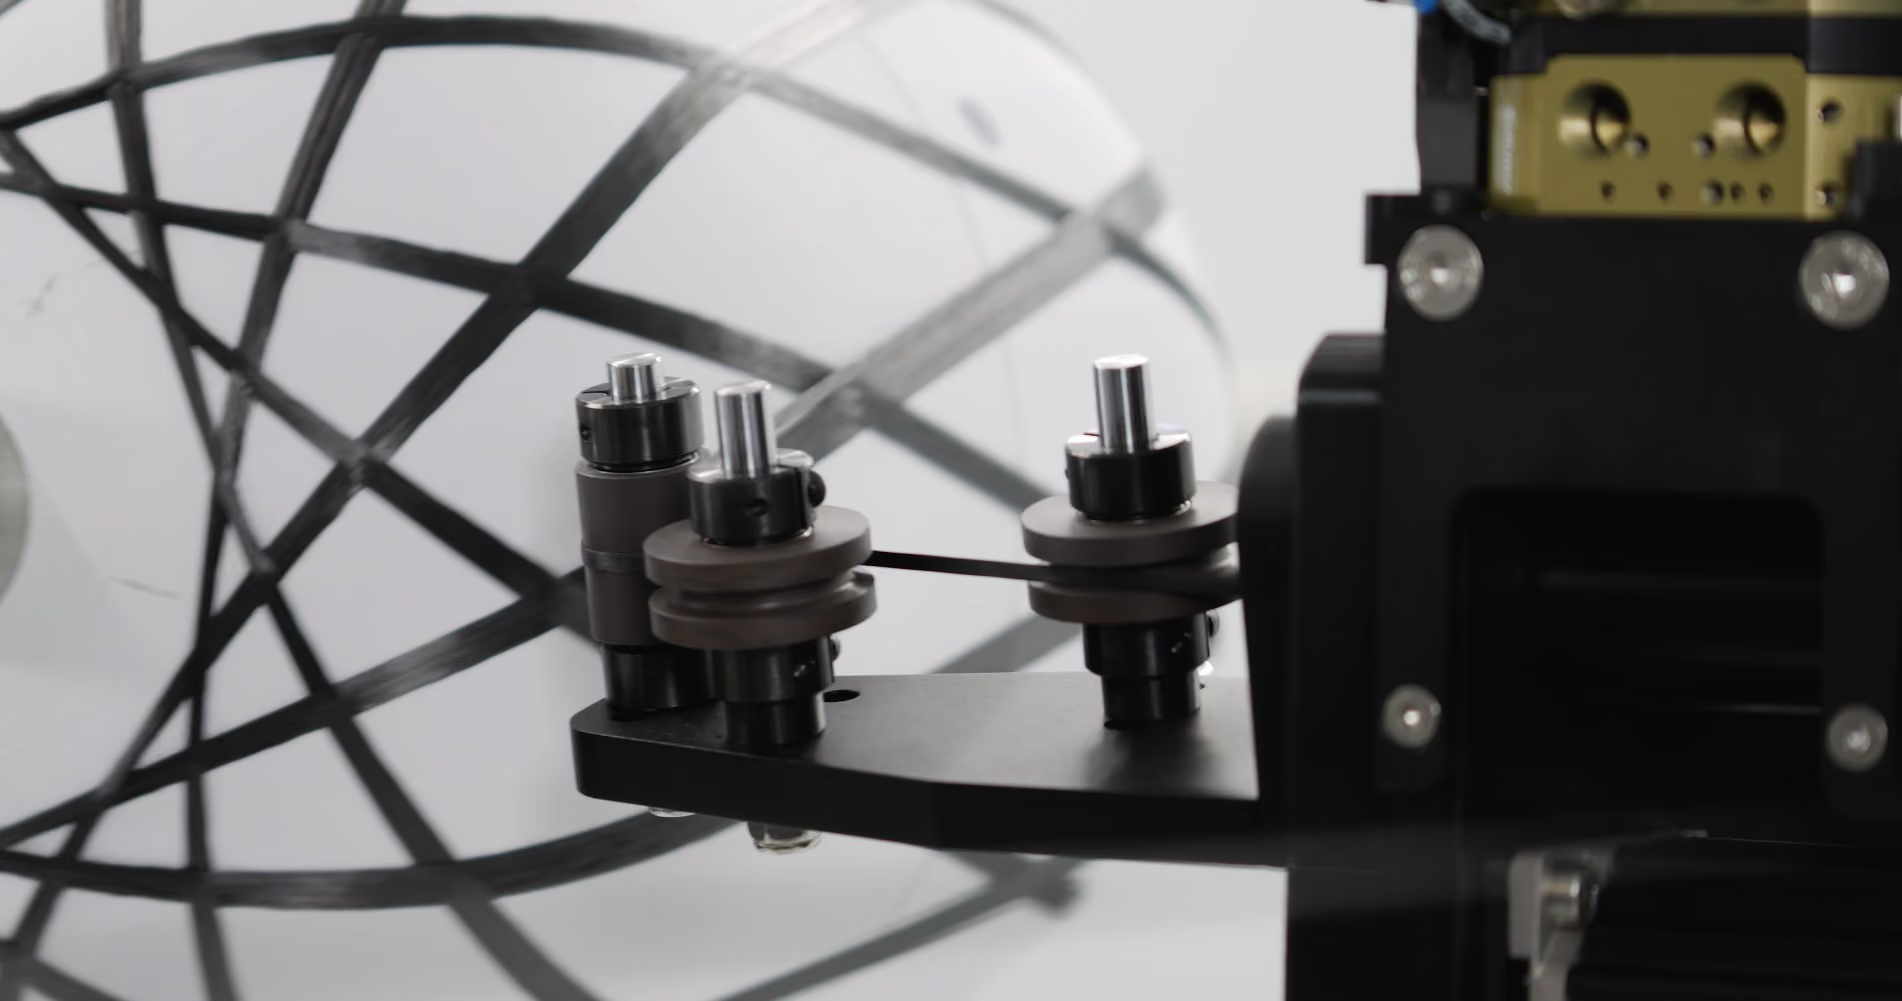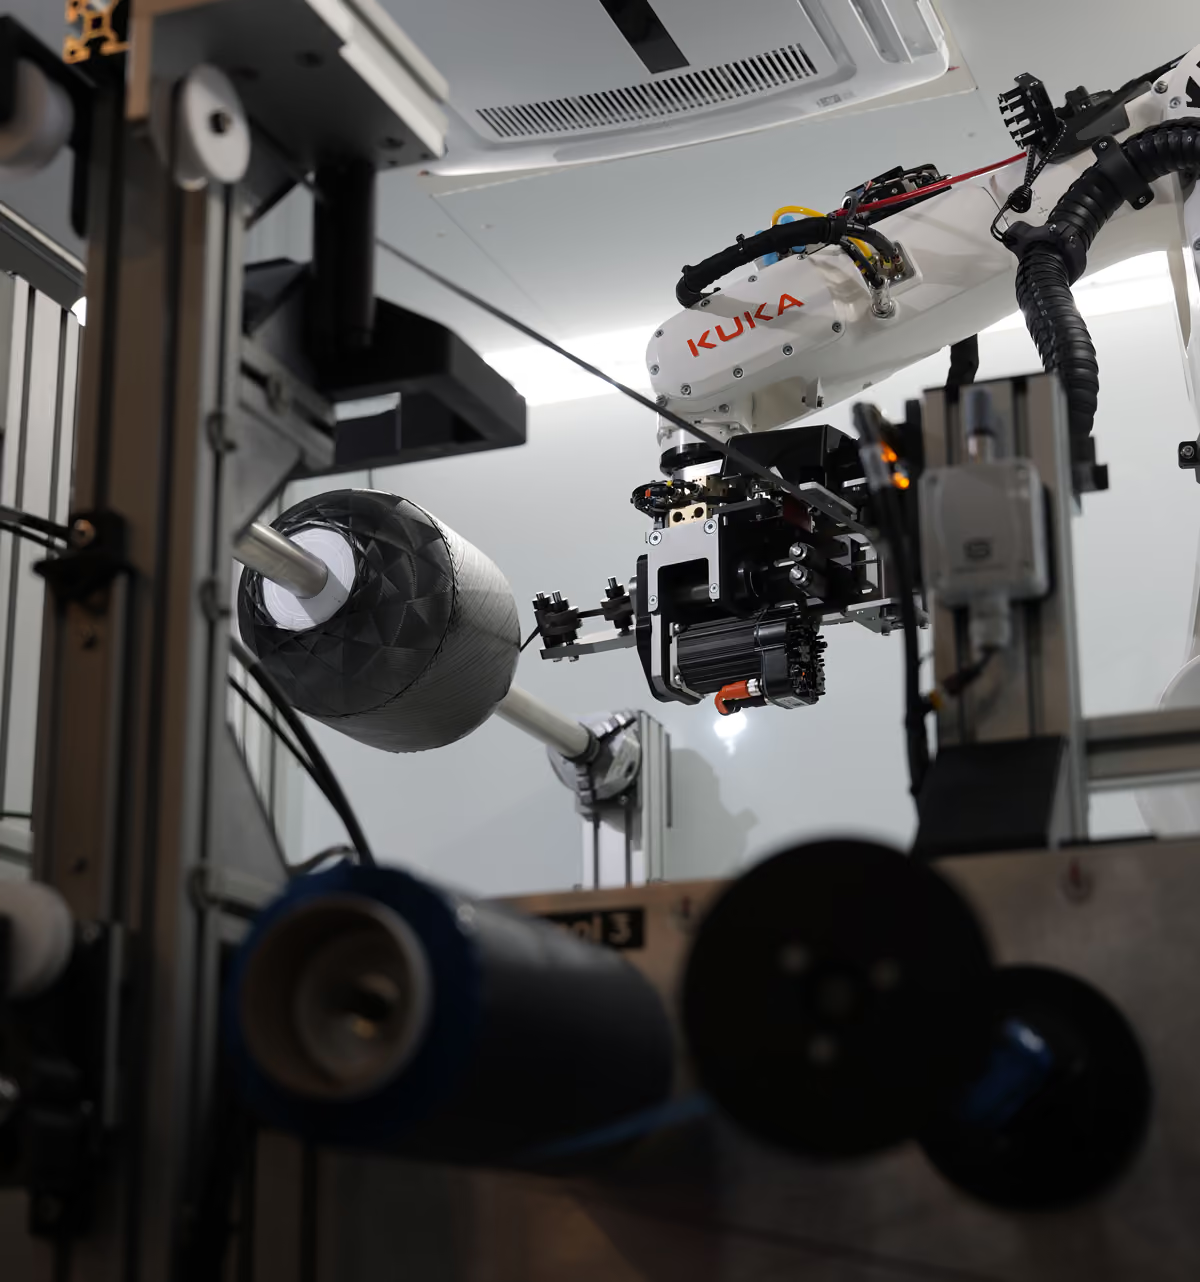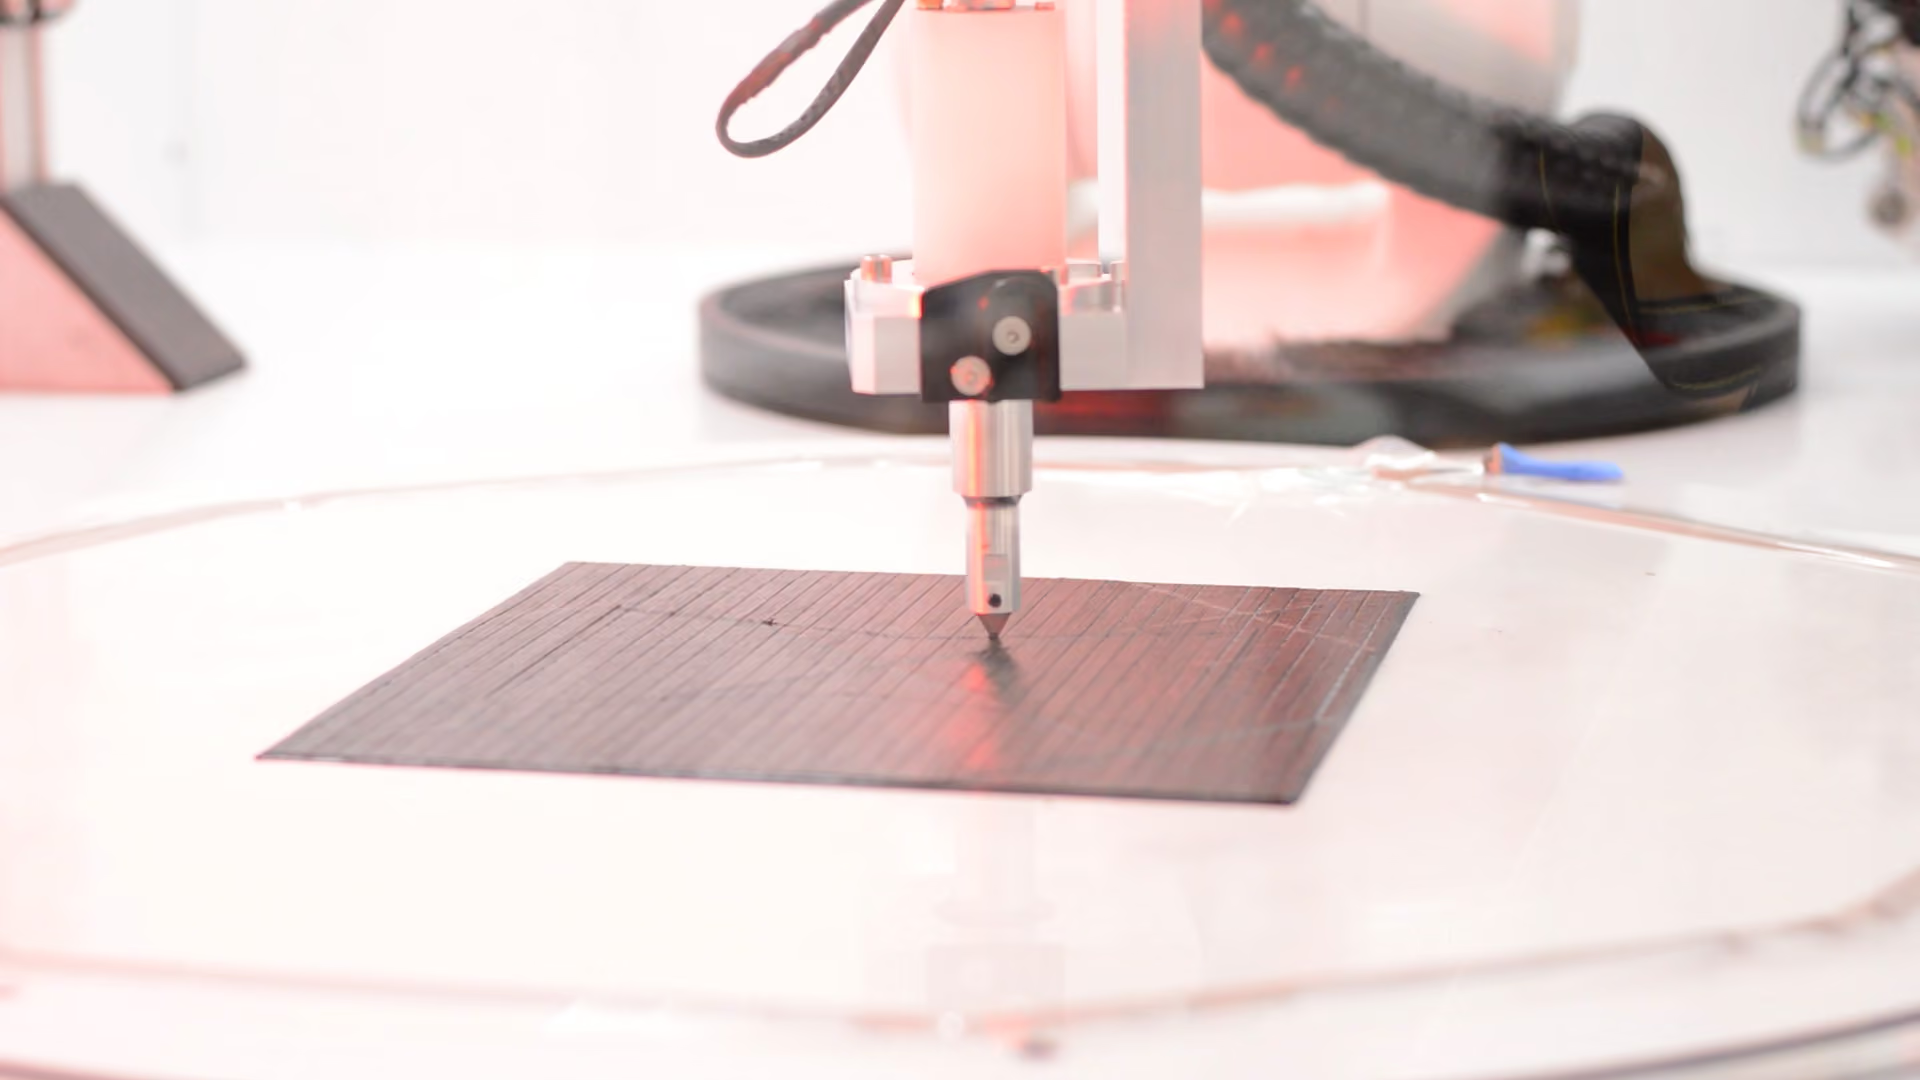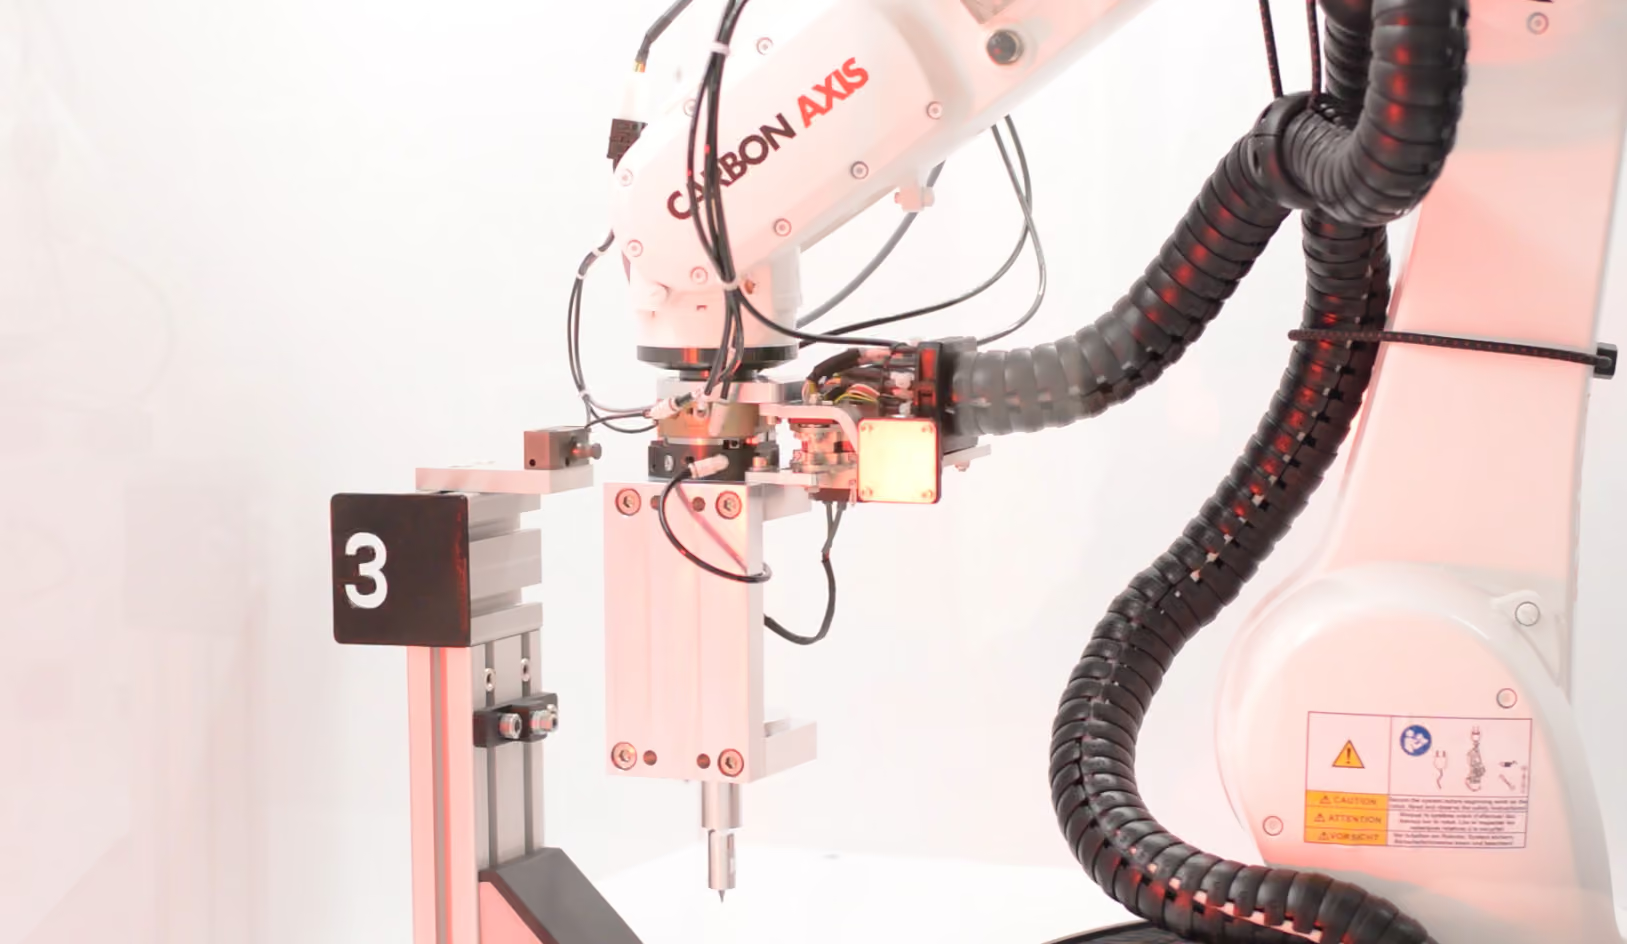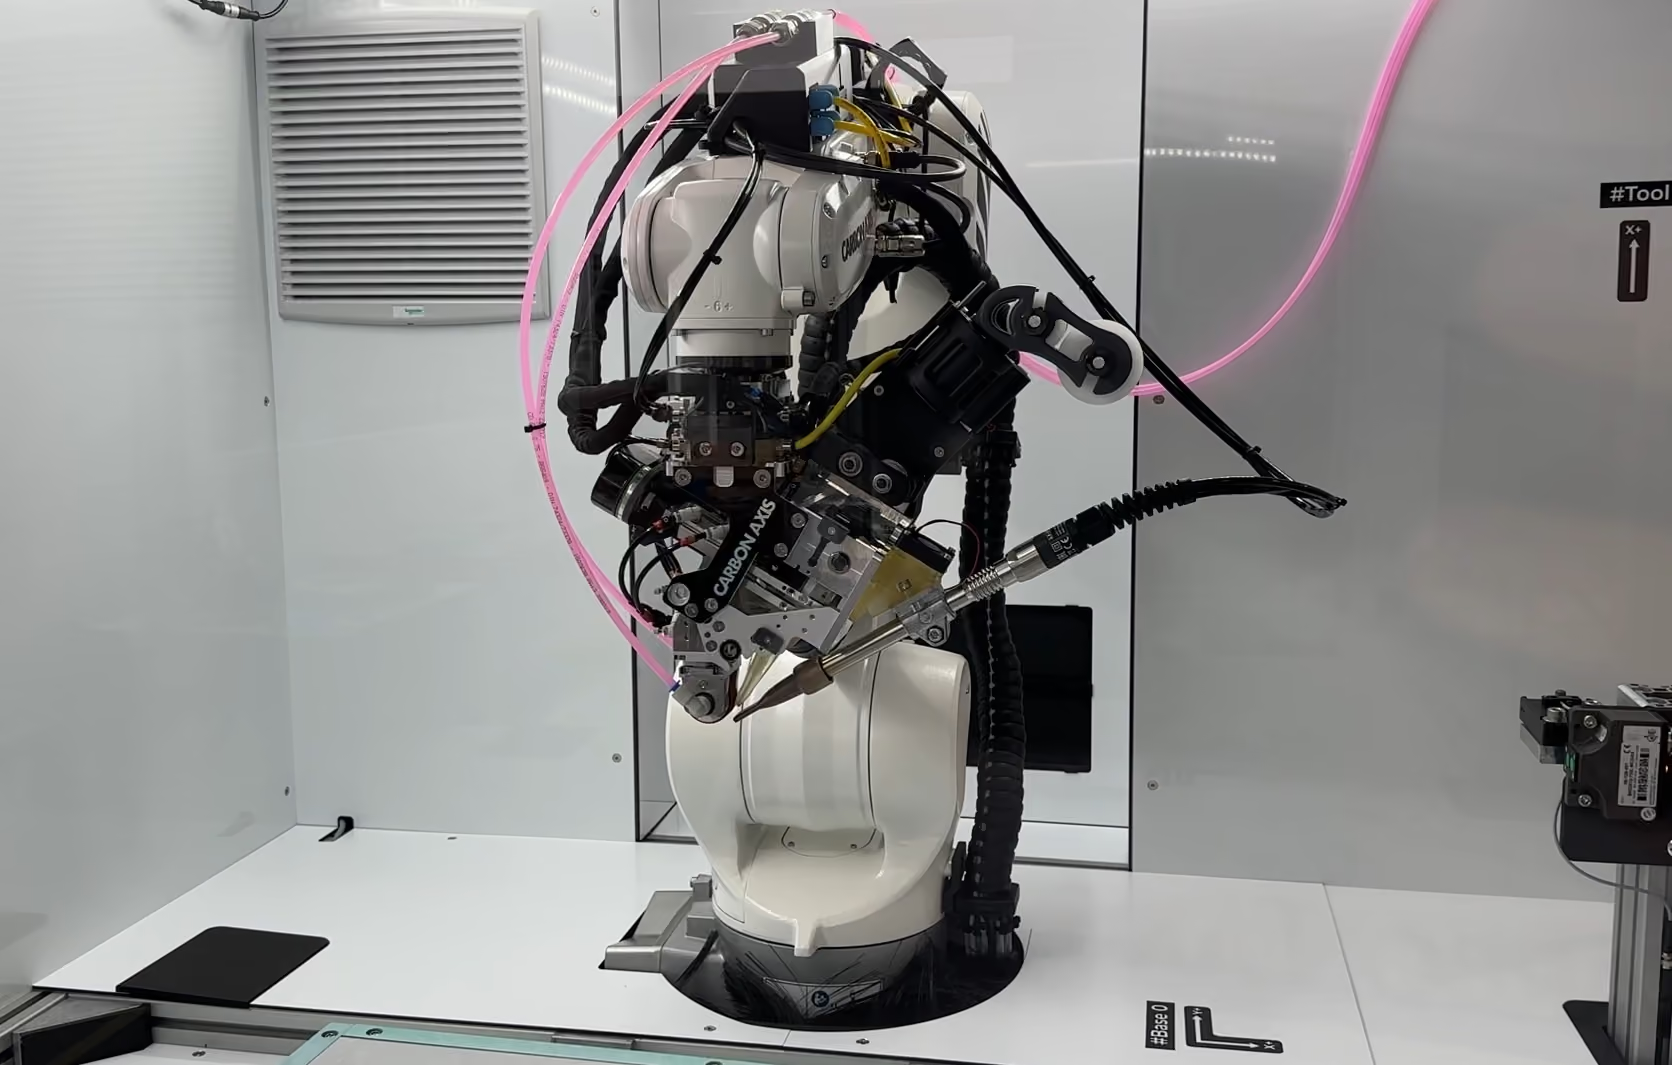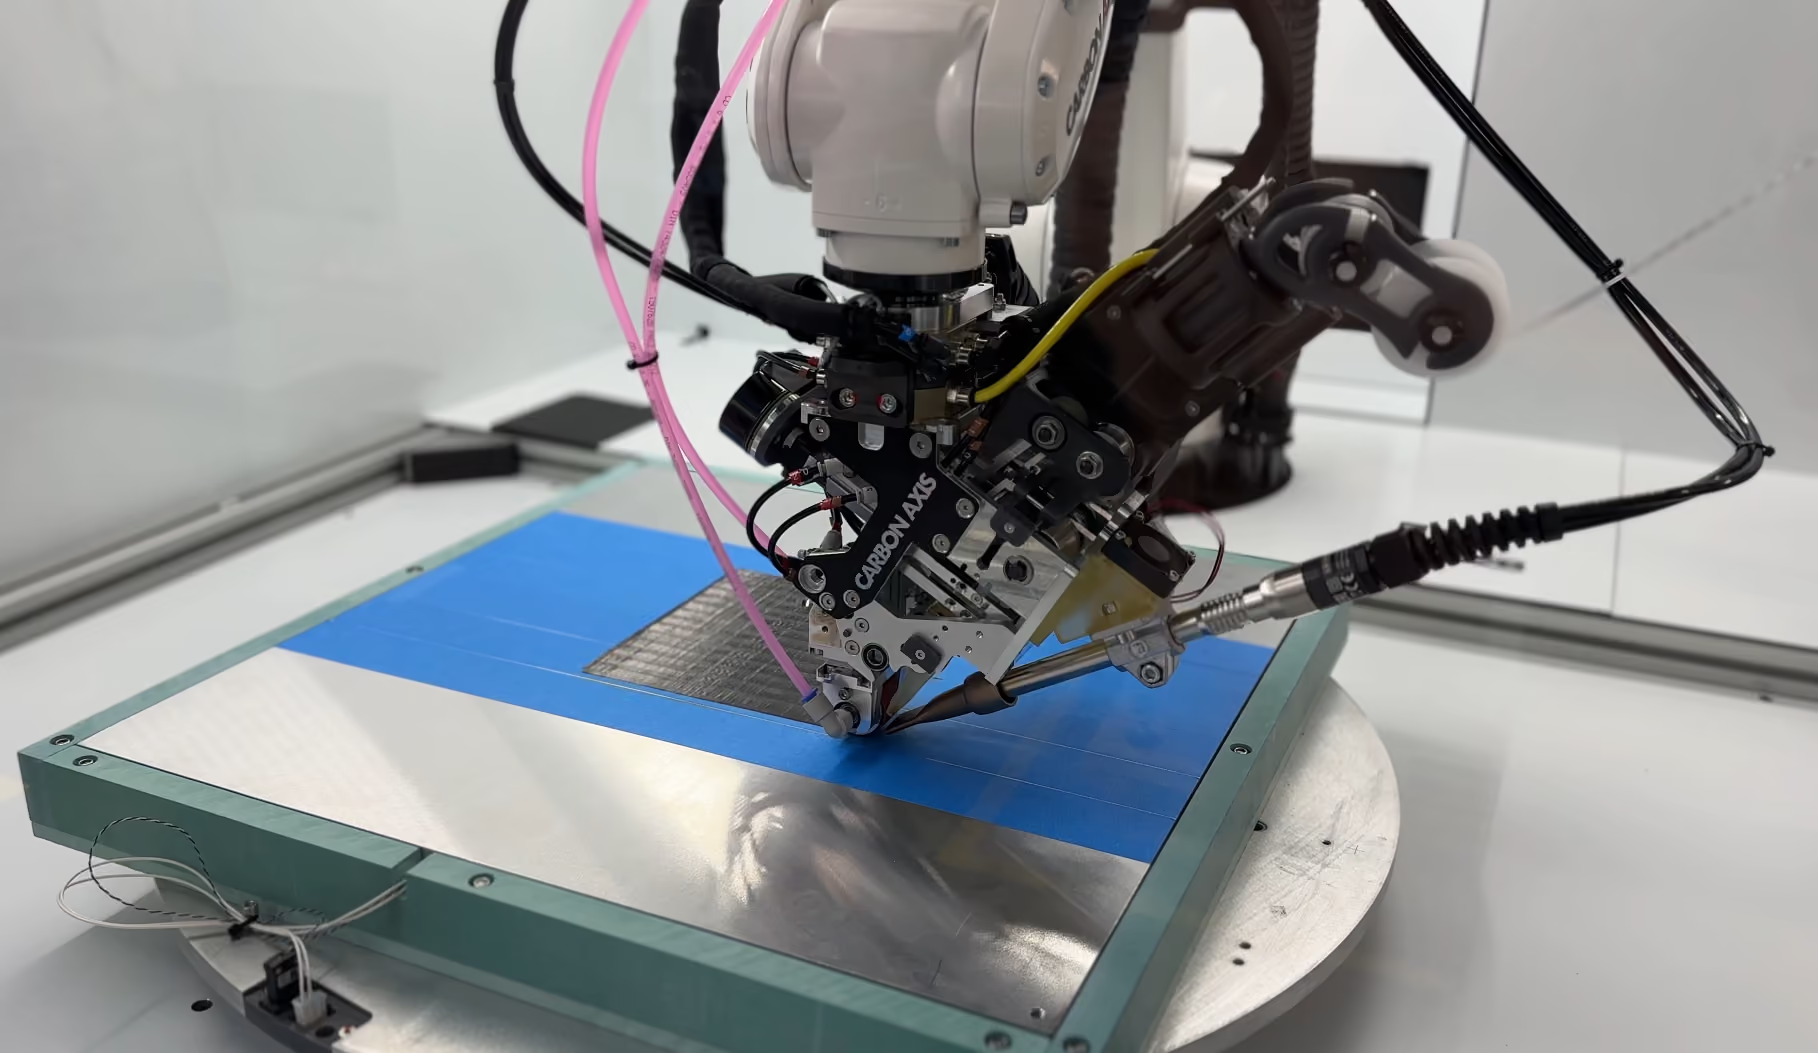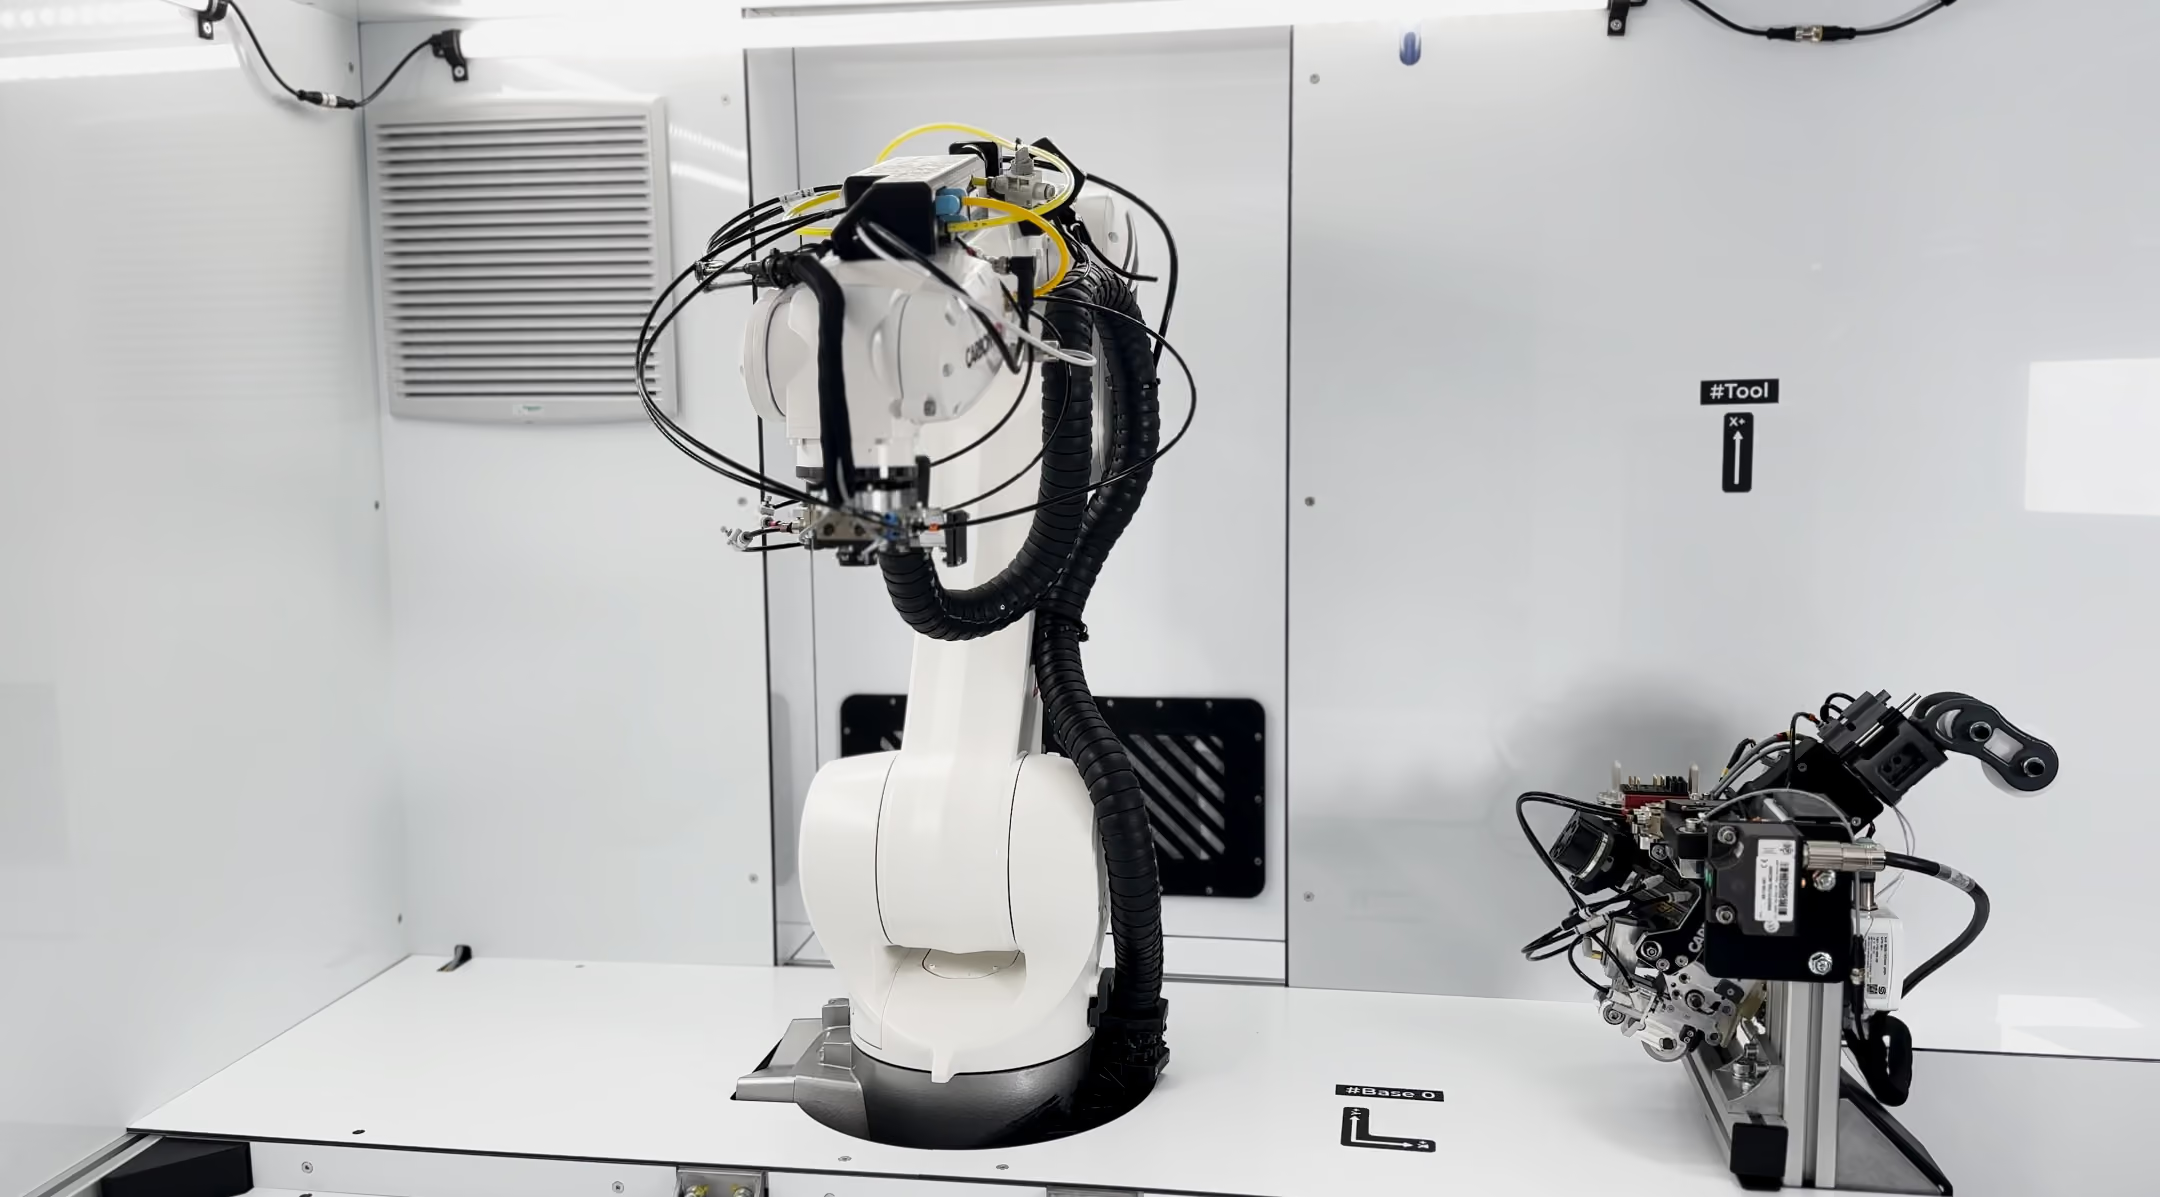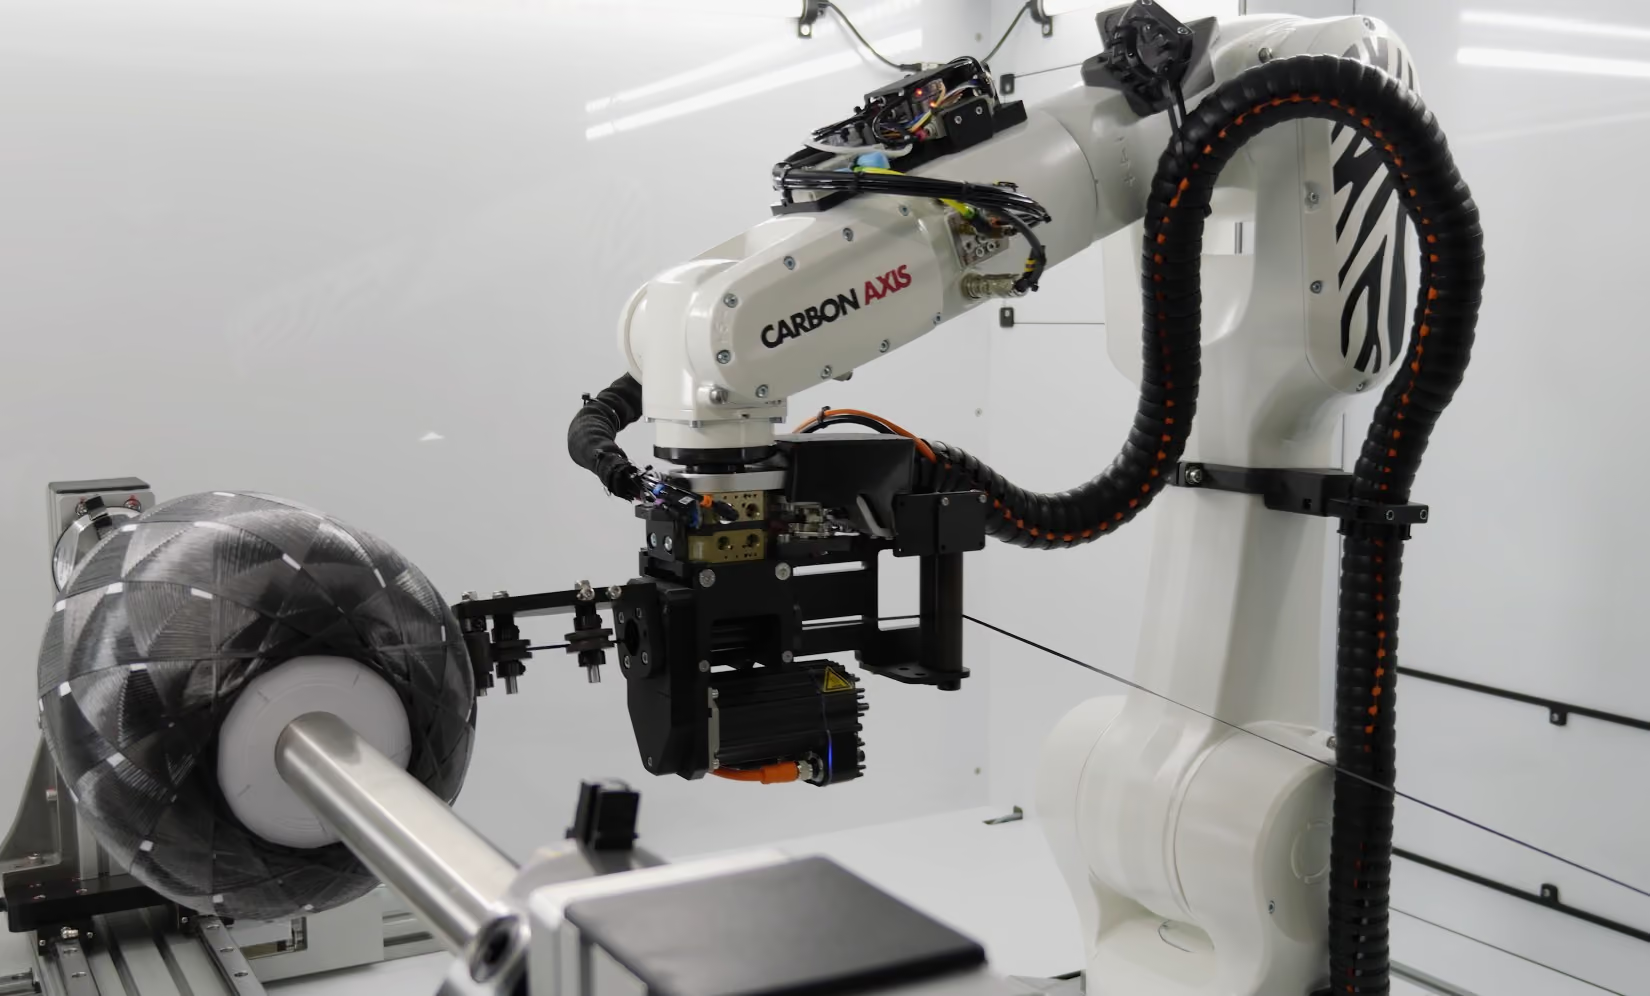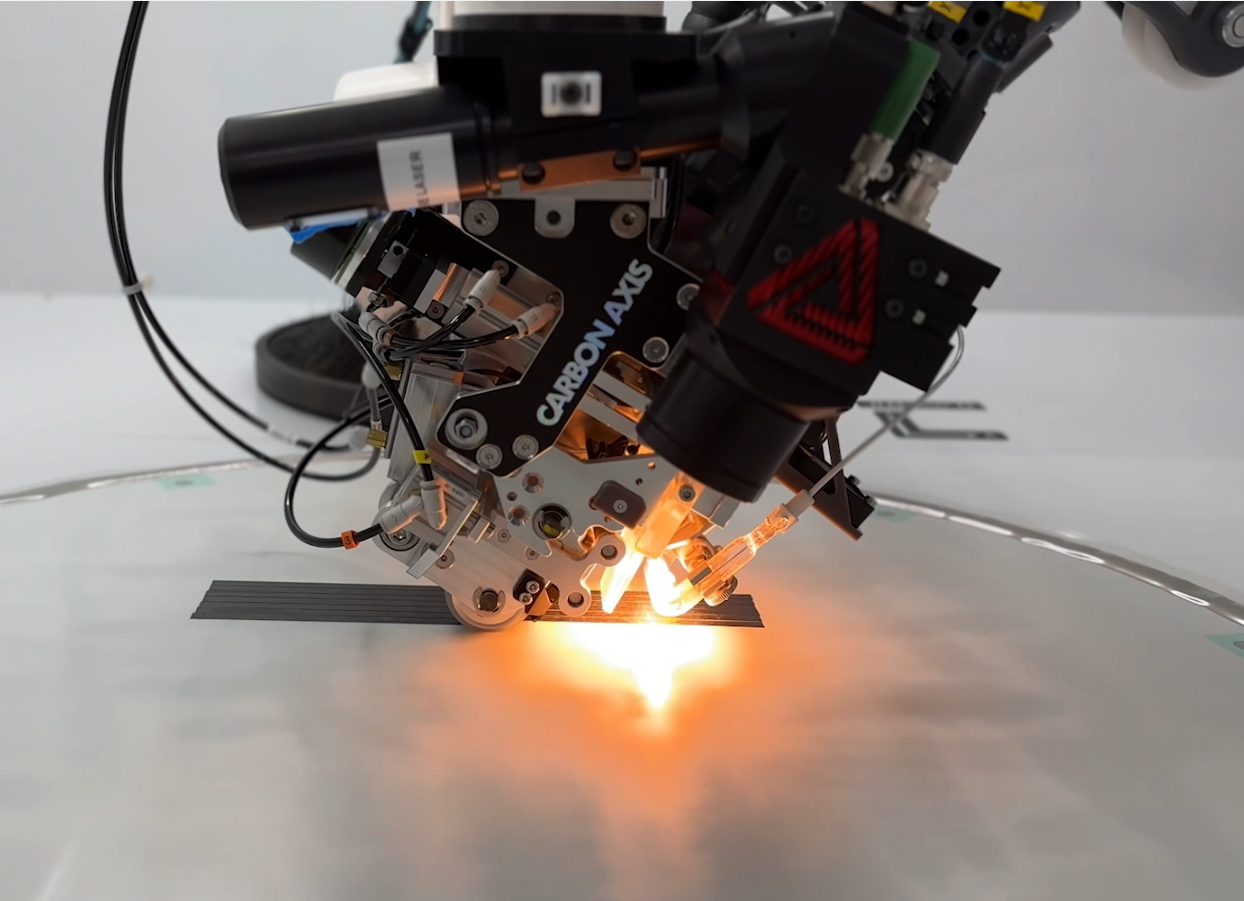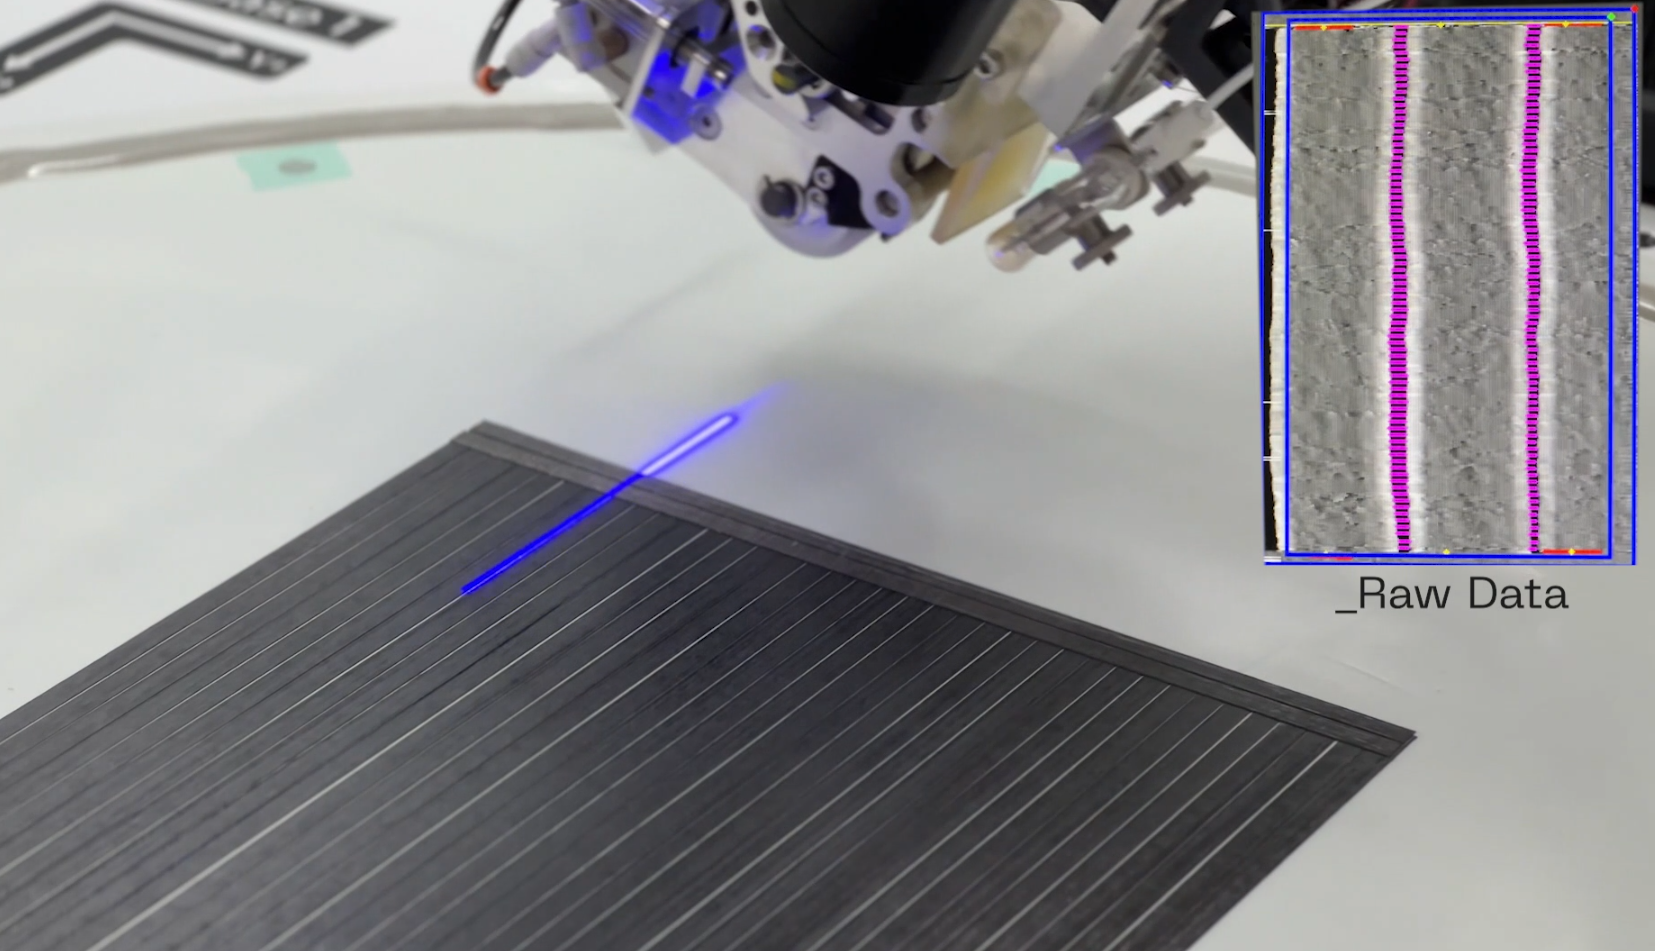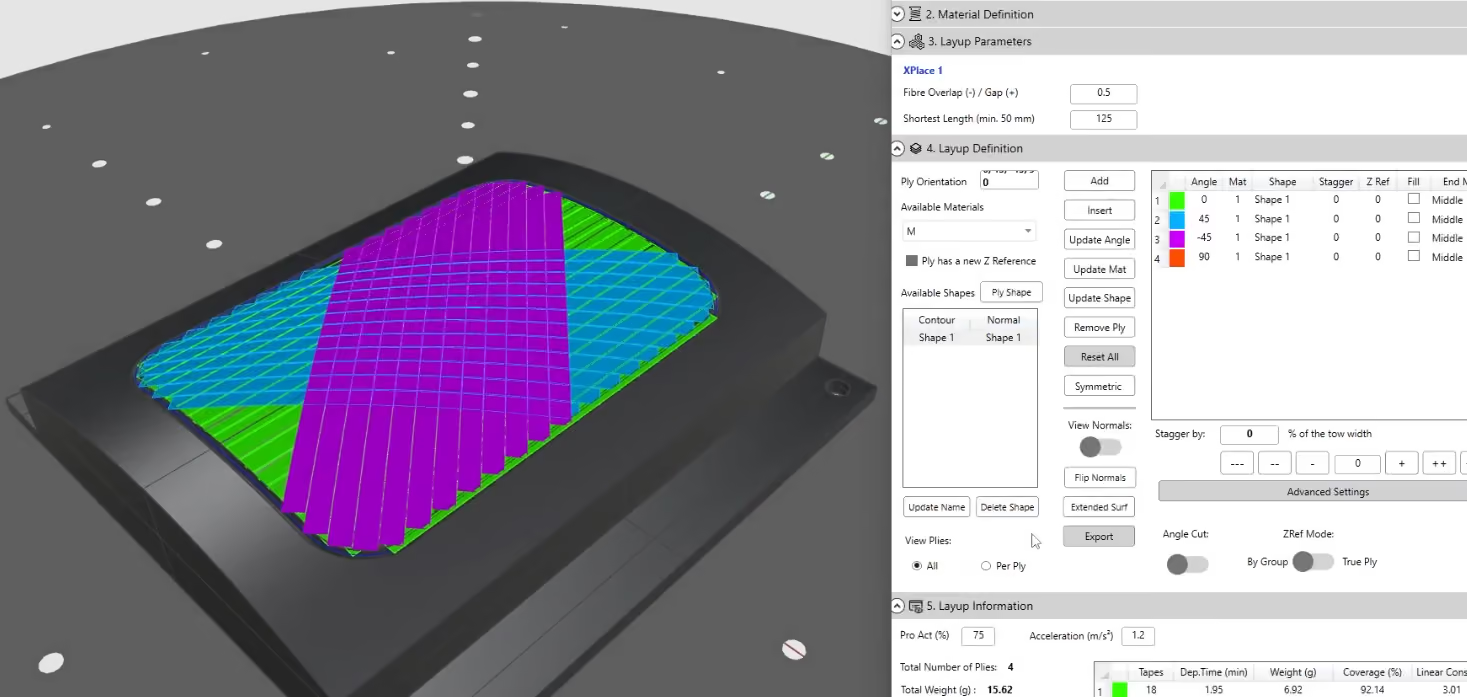
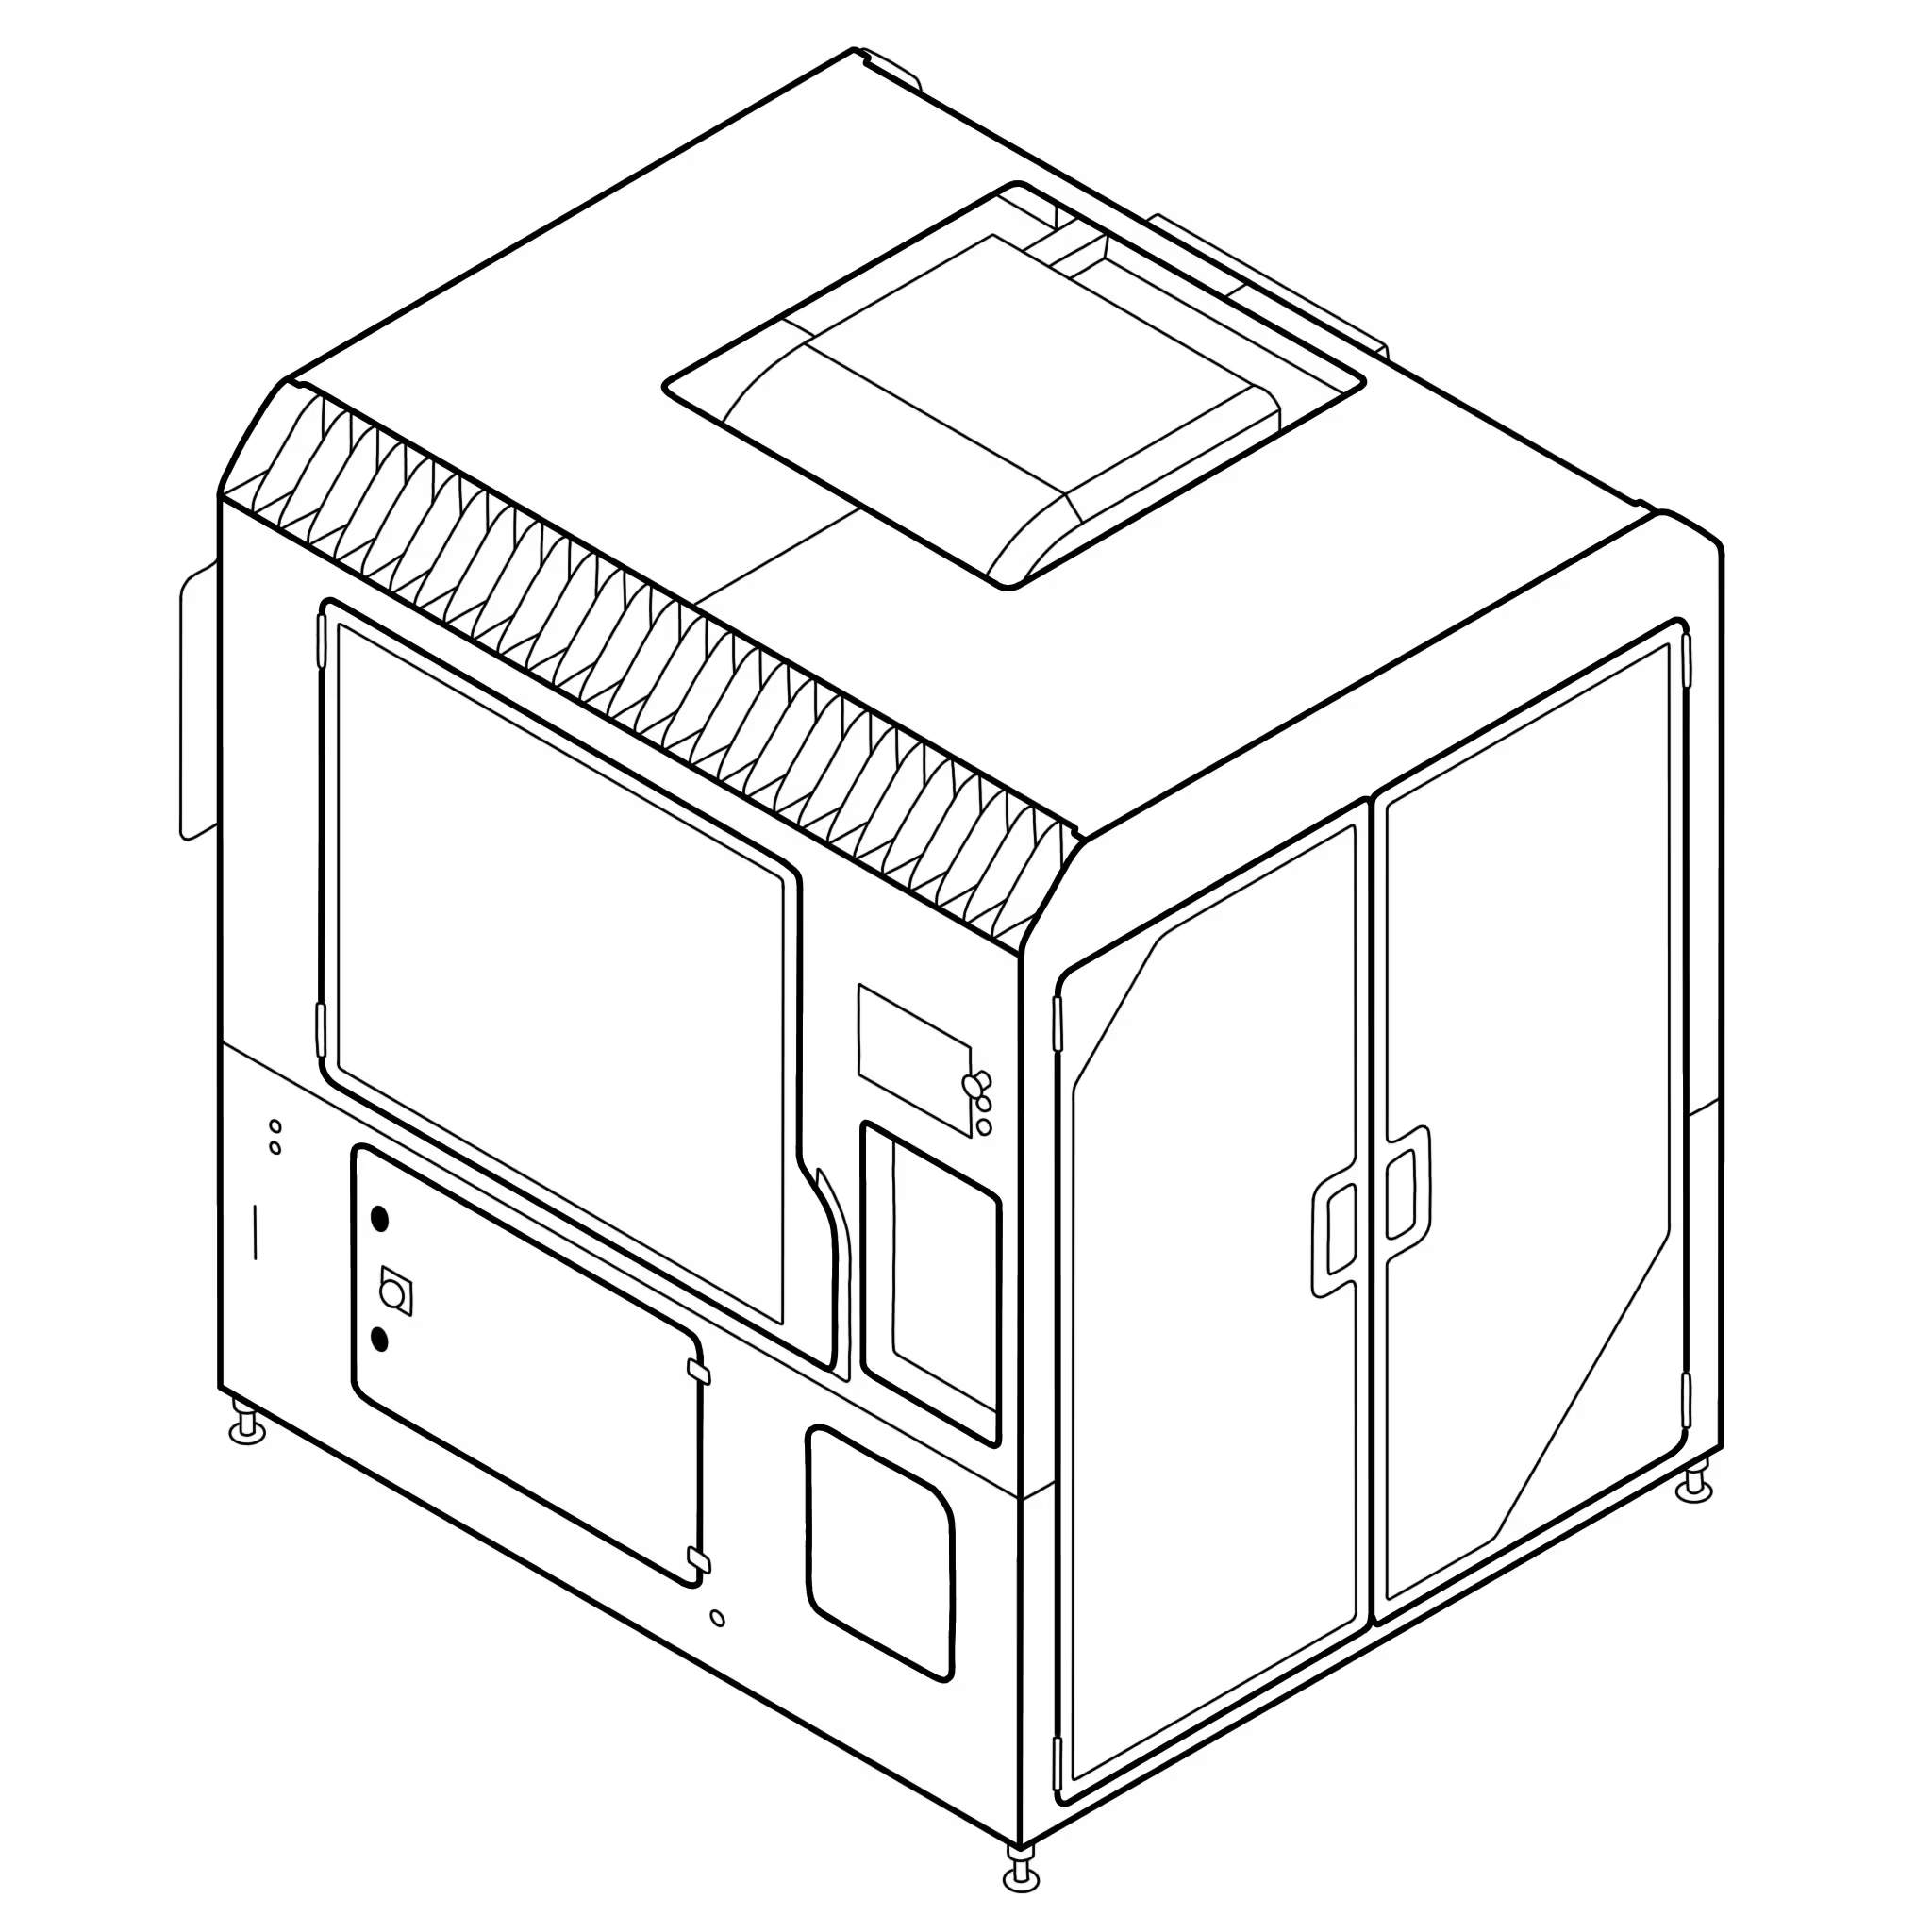
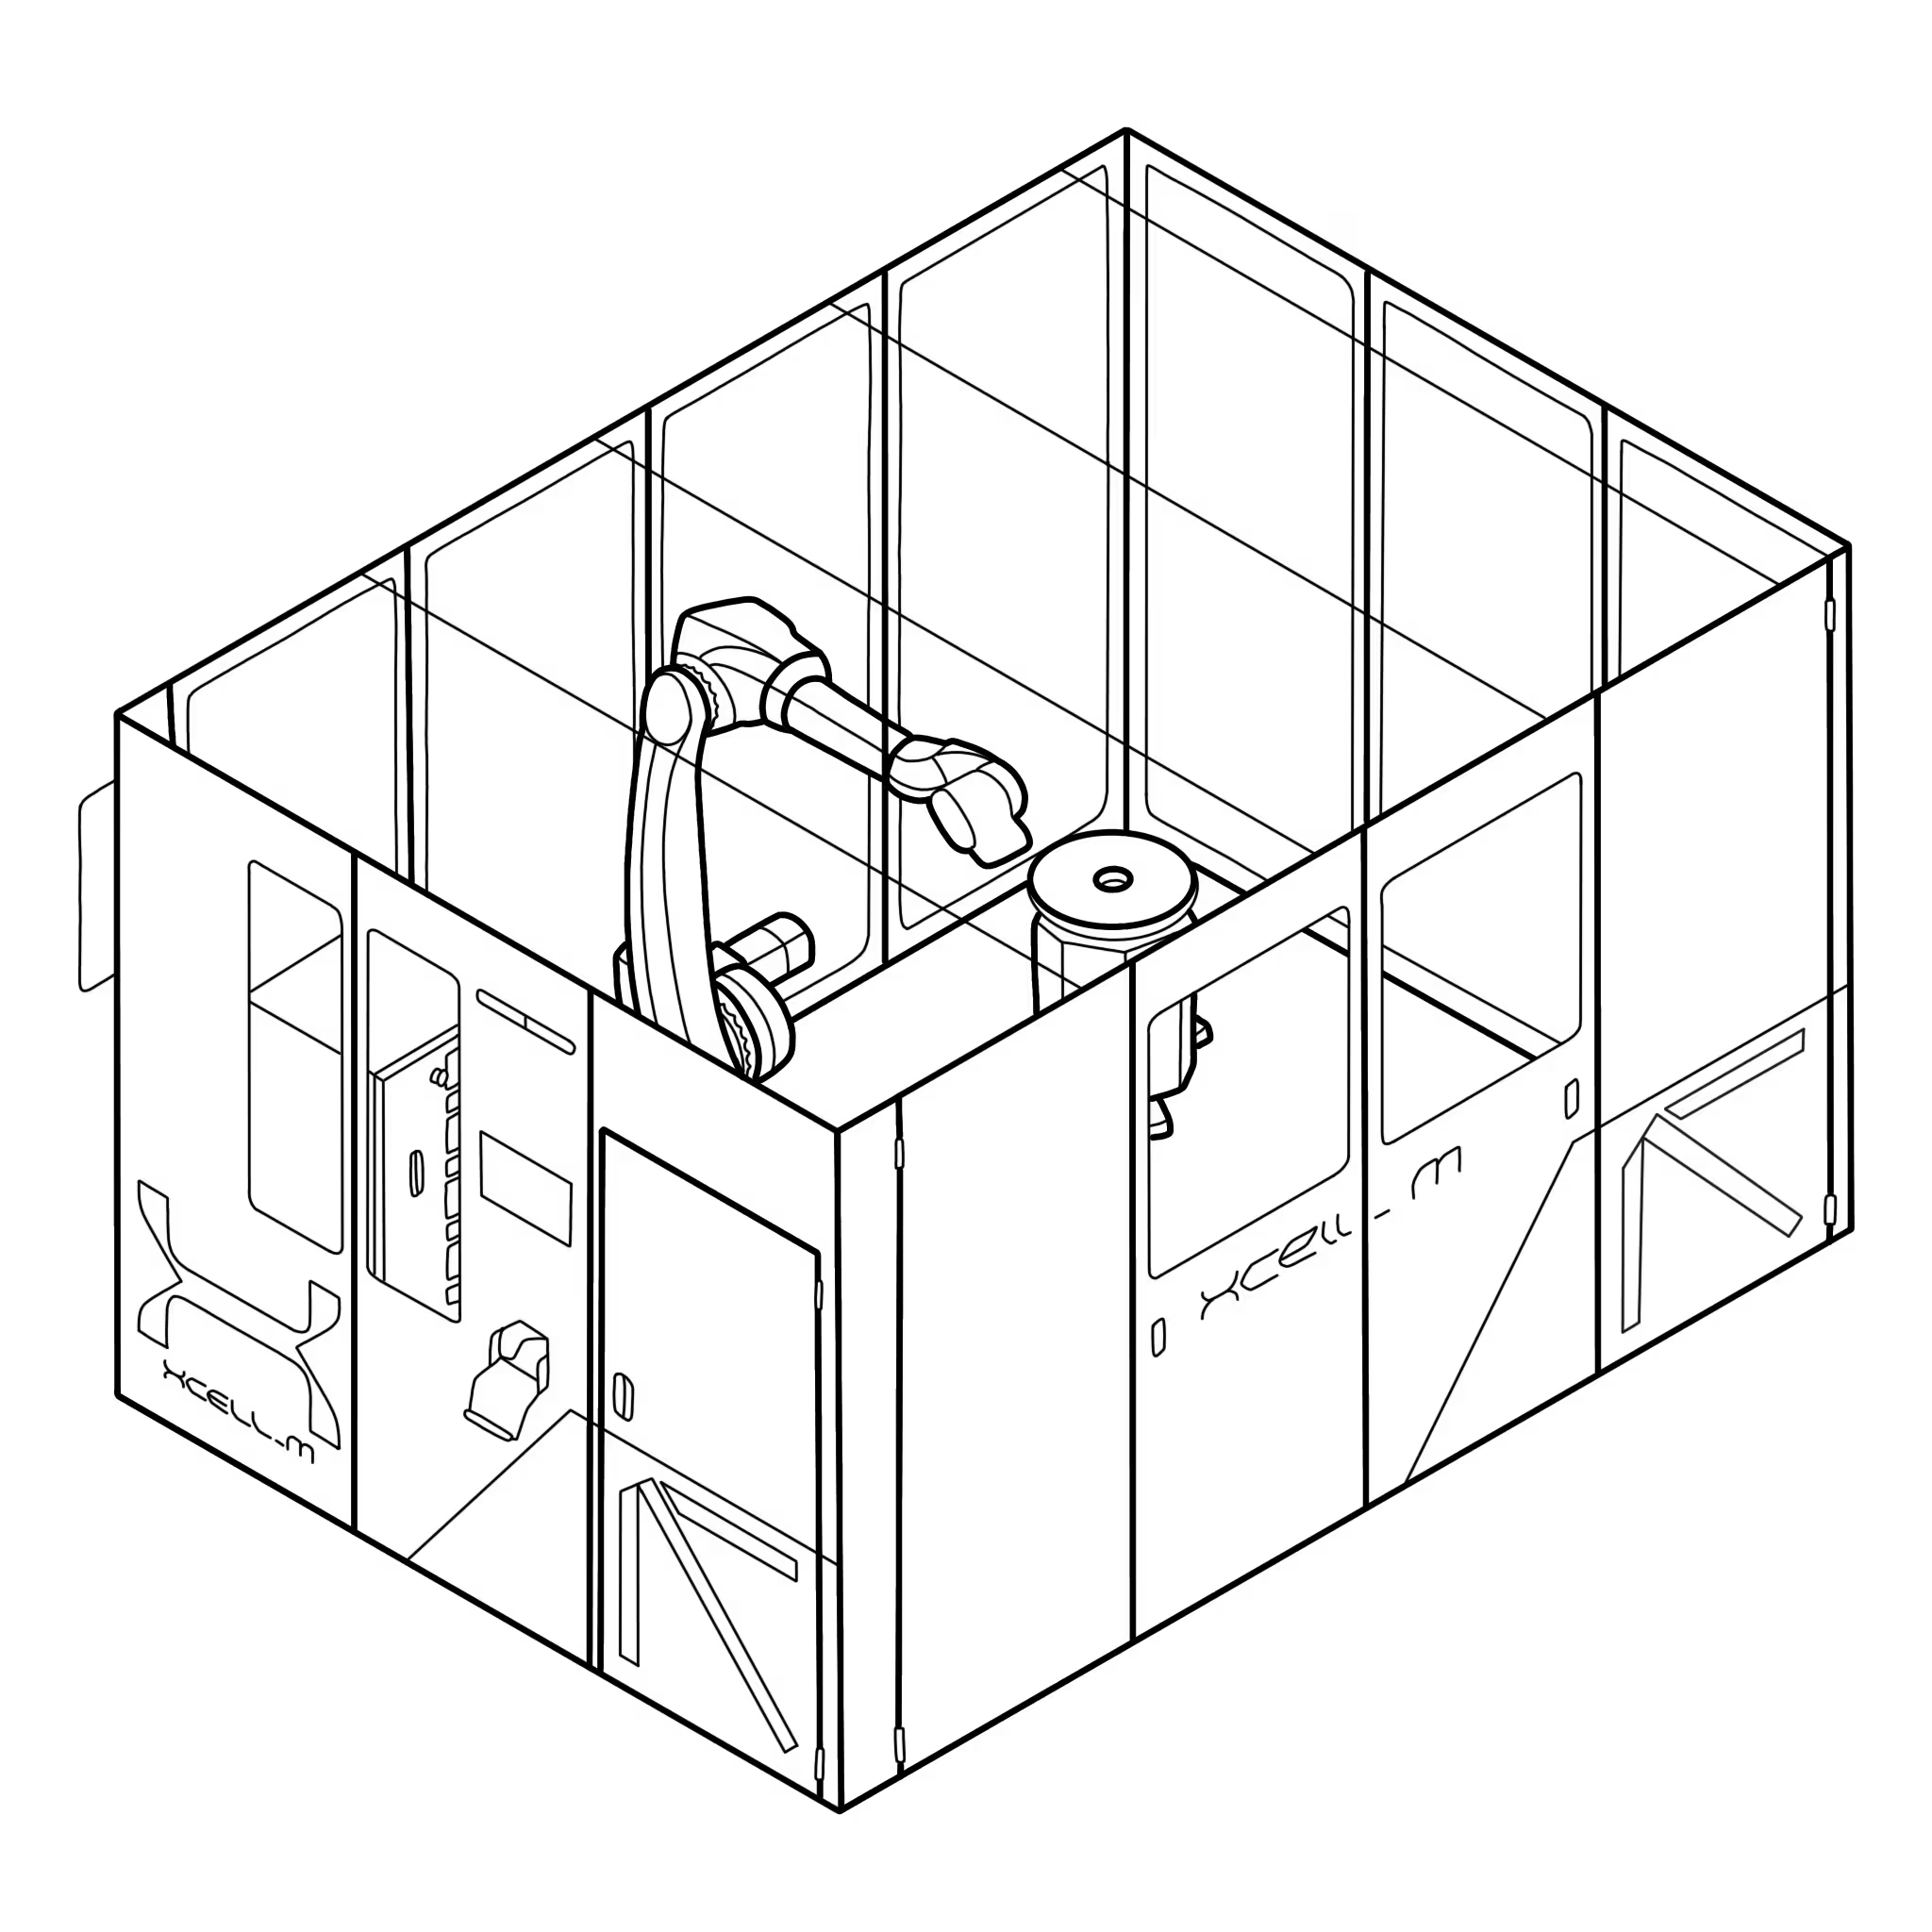
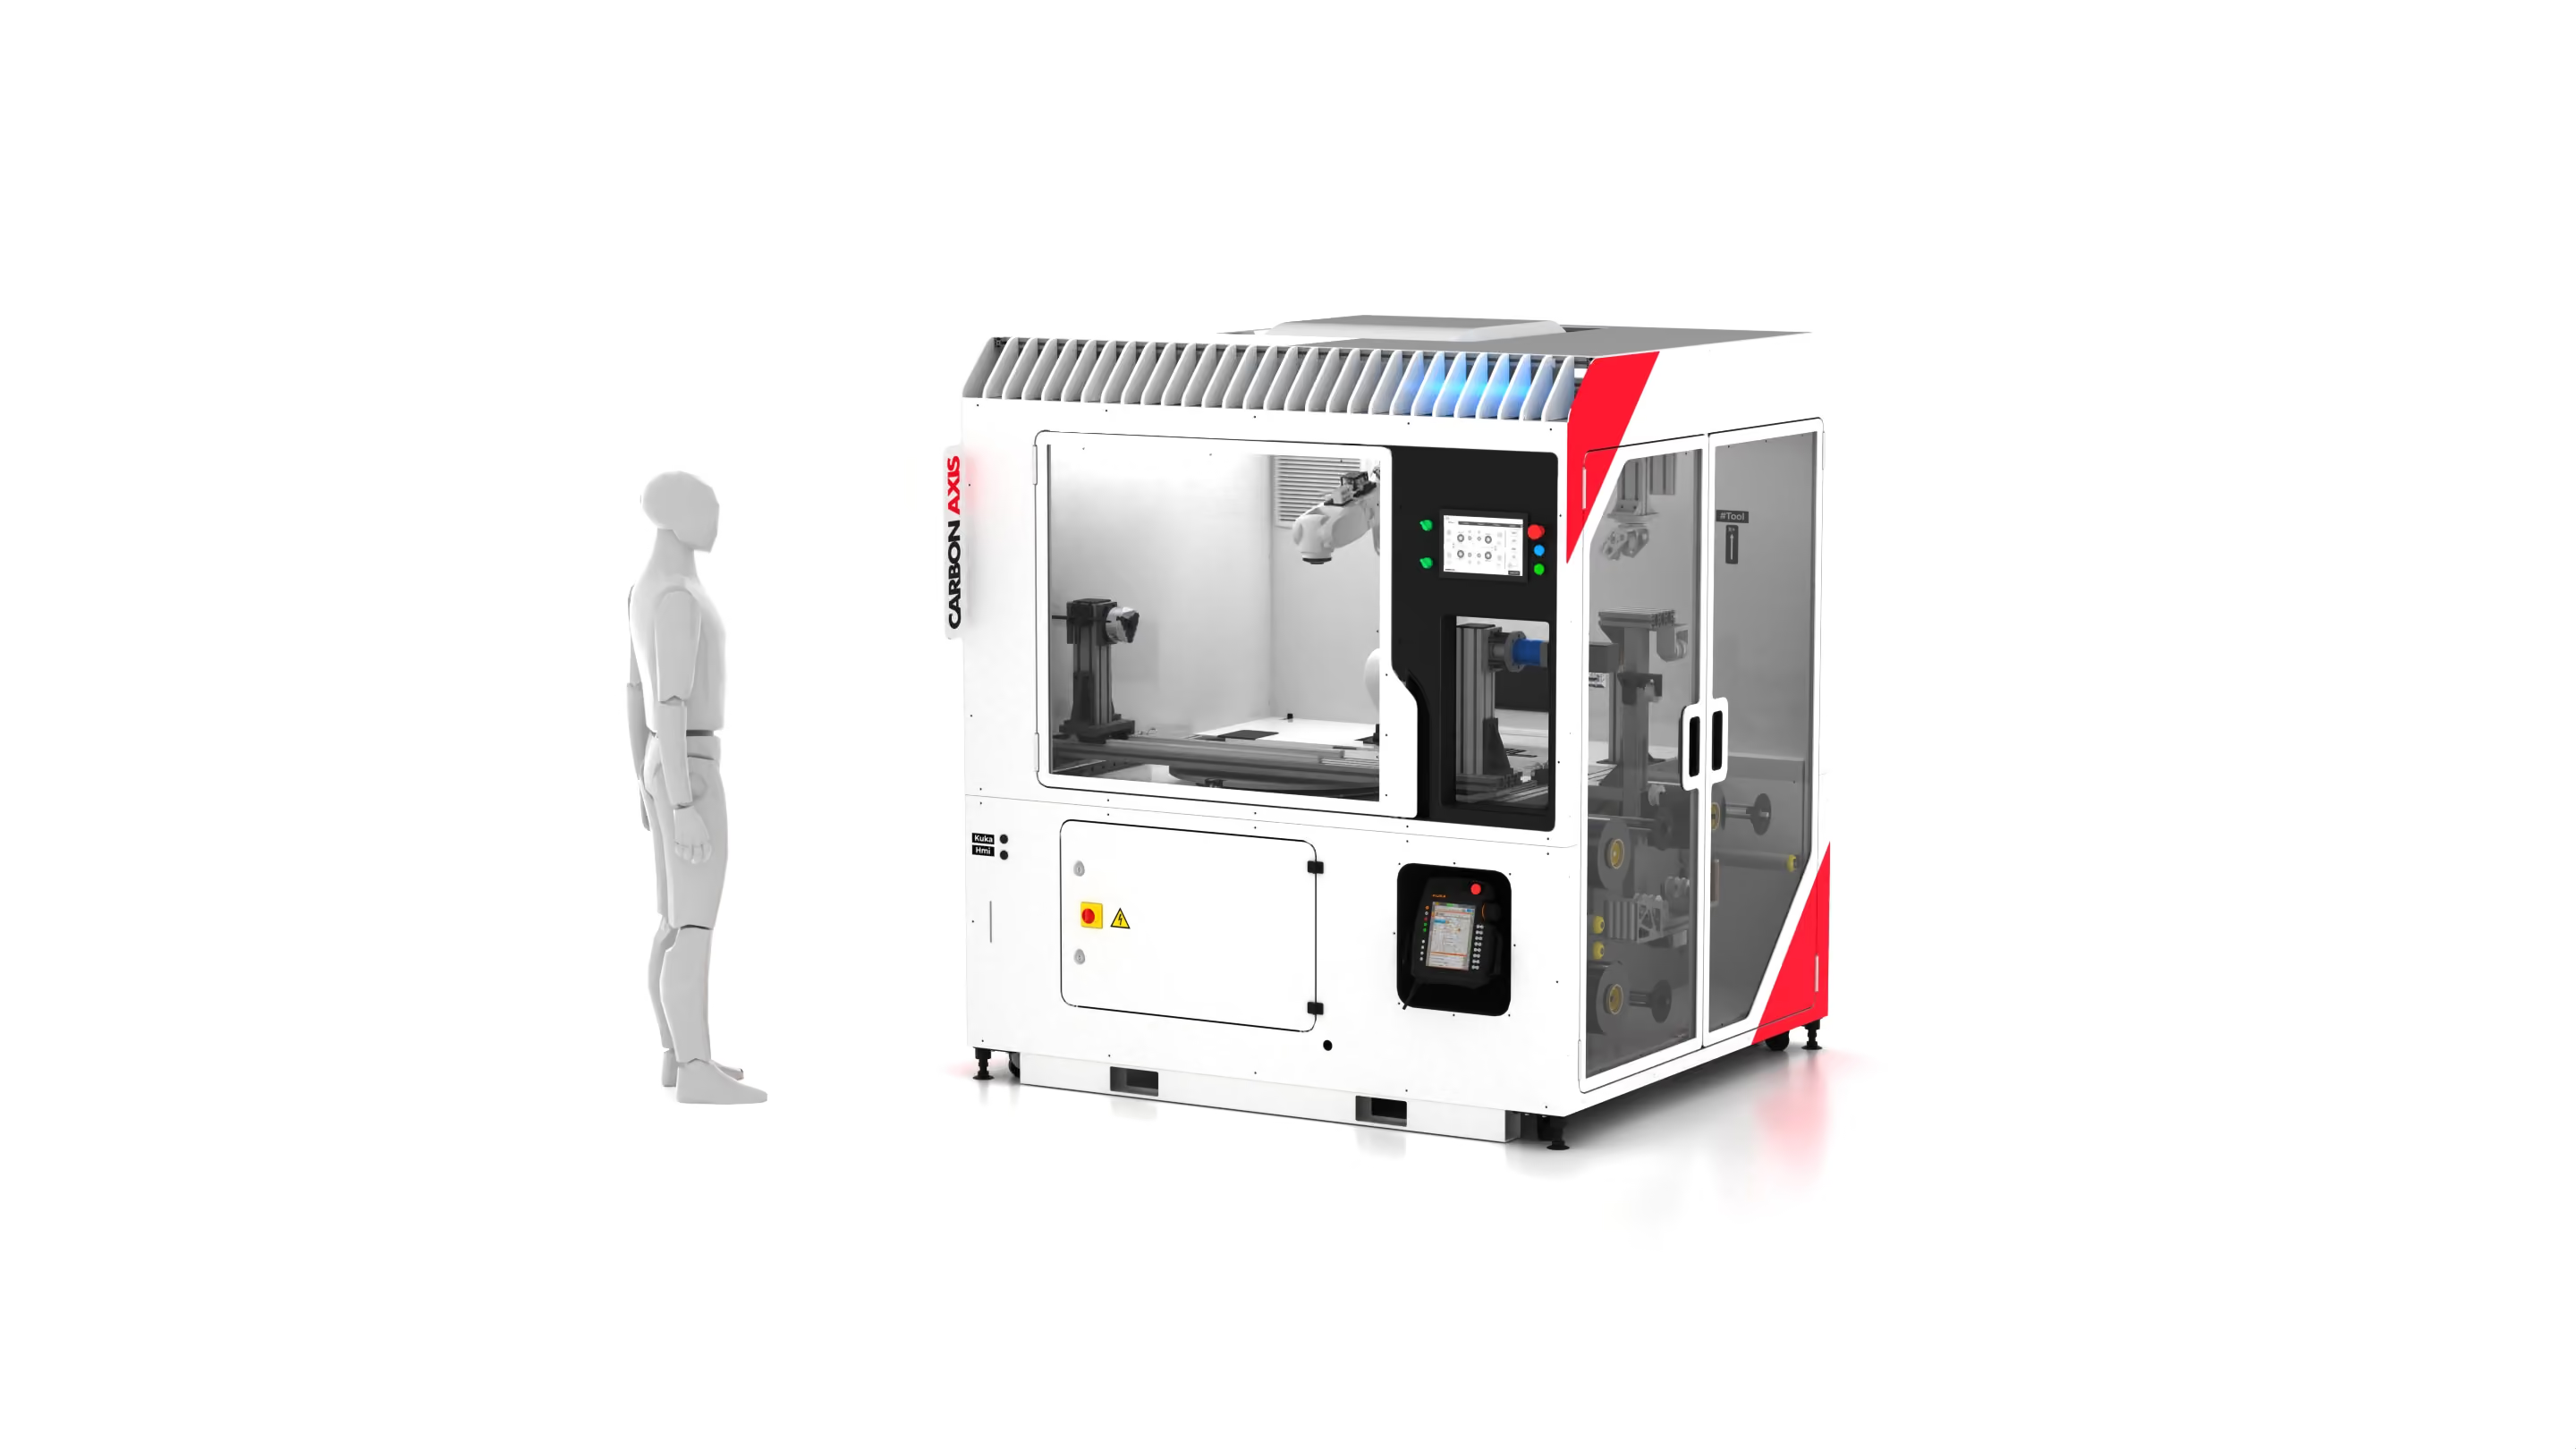
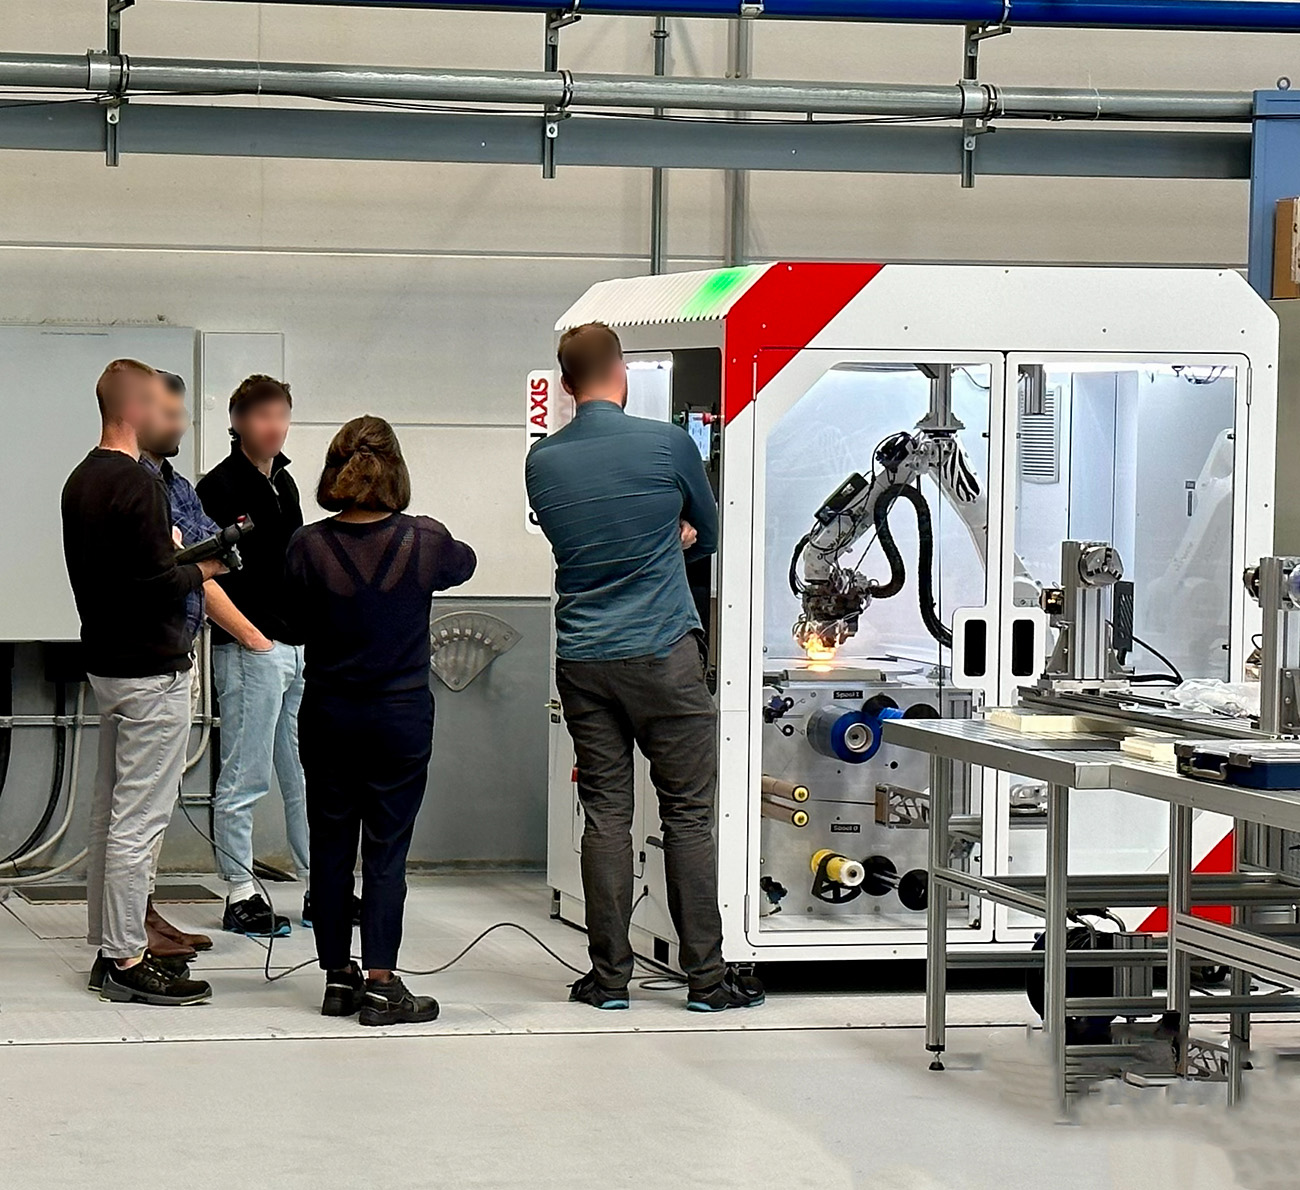
The machine designed to kickstart your automated journey. From Research and Development to the production of small parts, the XCell is the most compact multi process AFP machine in our range.
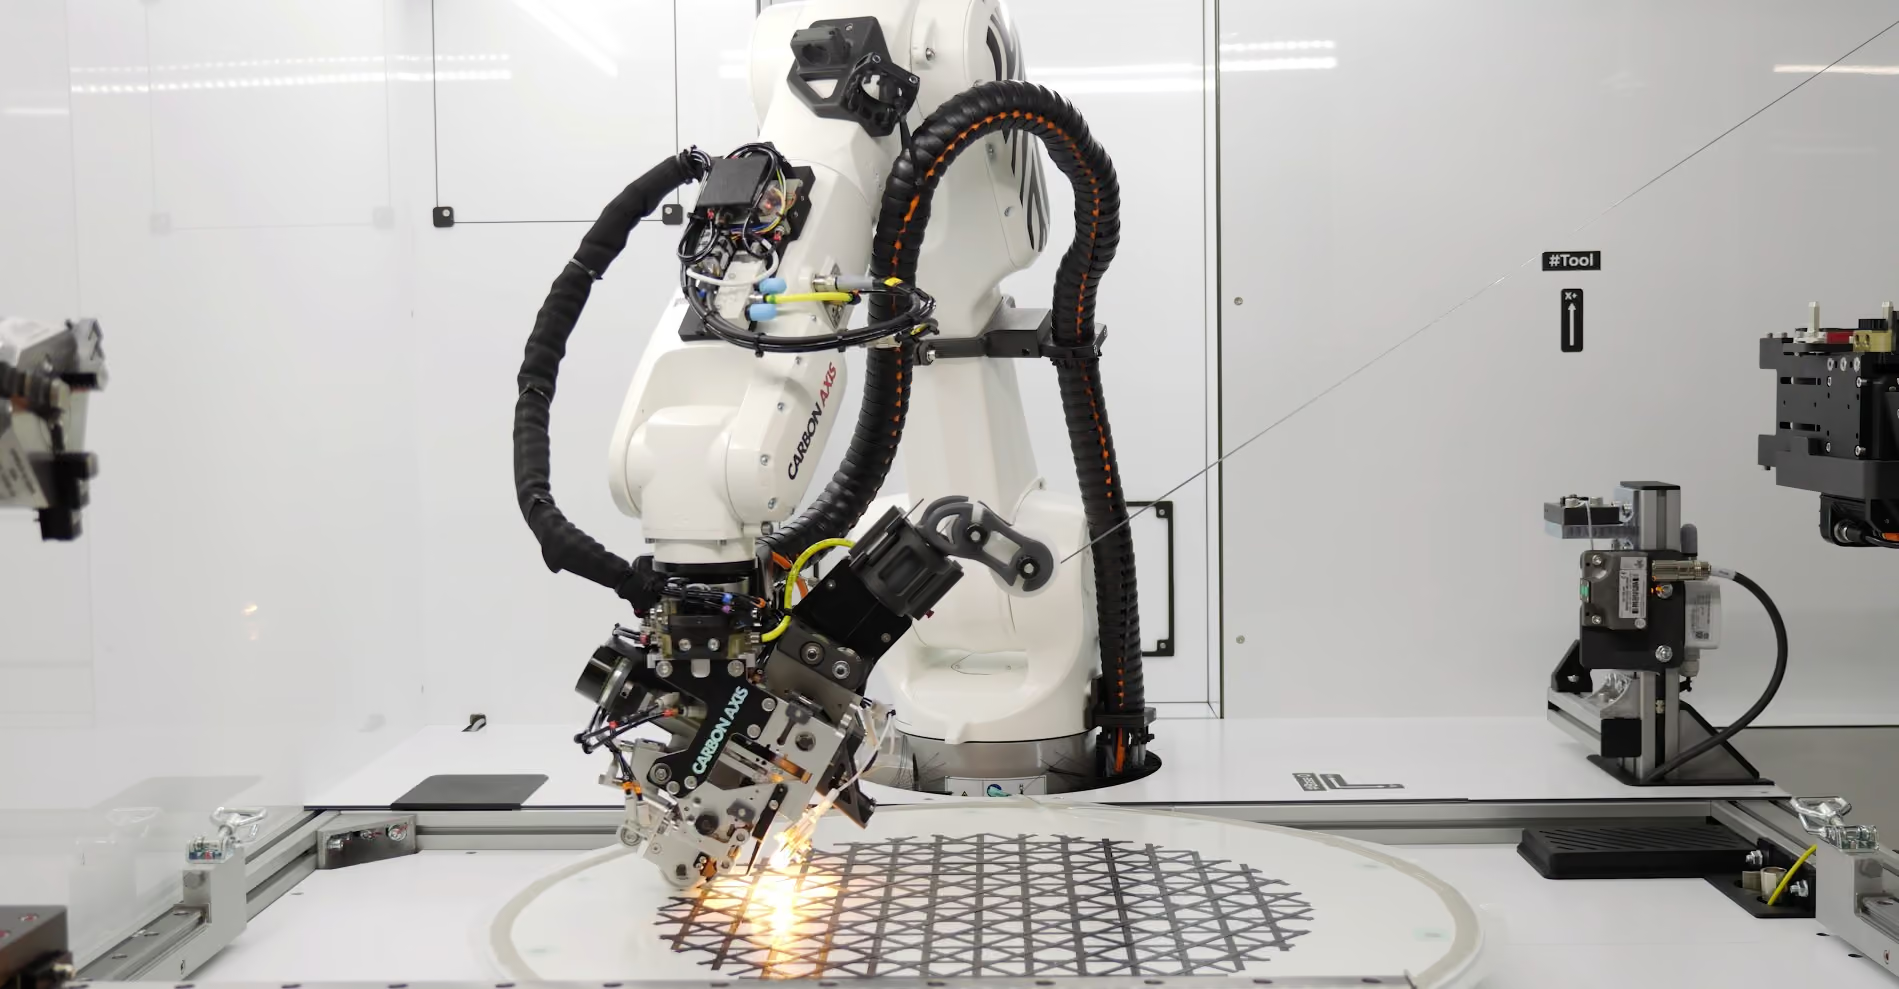
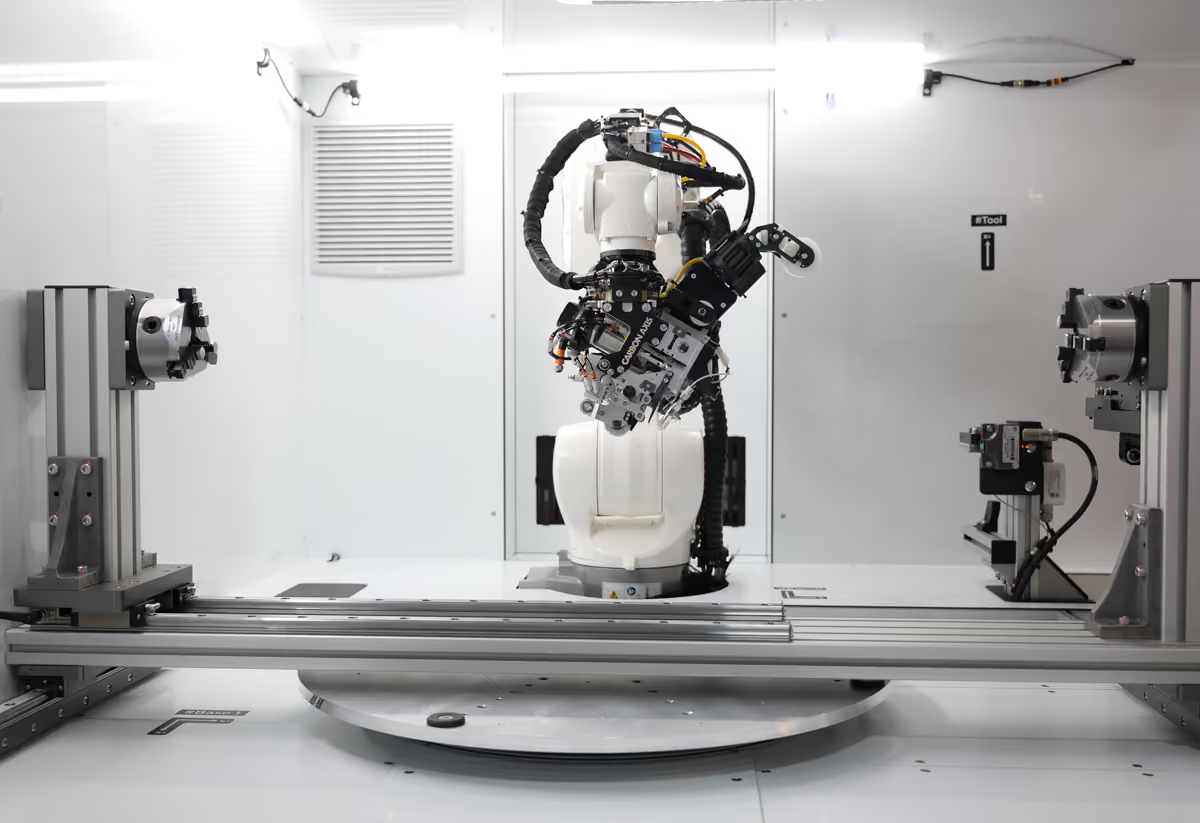
Cell configuration
Dimensions: 1.9m x 1.7 m x 2.1 m
Temperature-controlled enclosure
Power :230 V single-phase
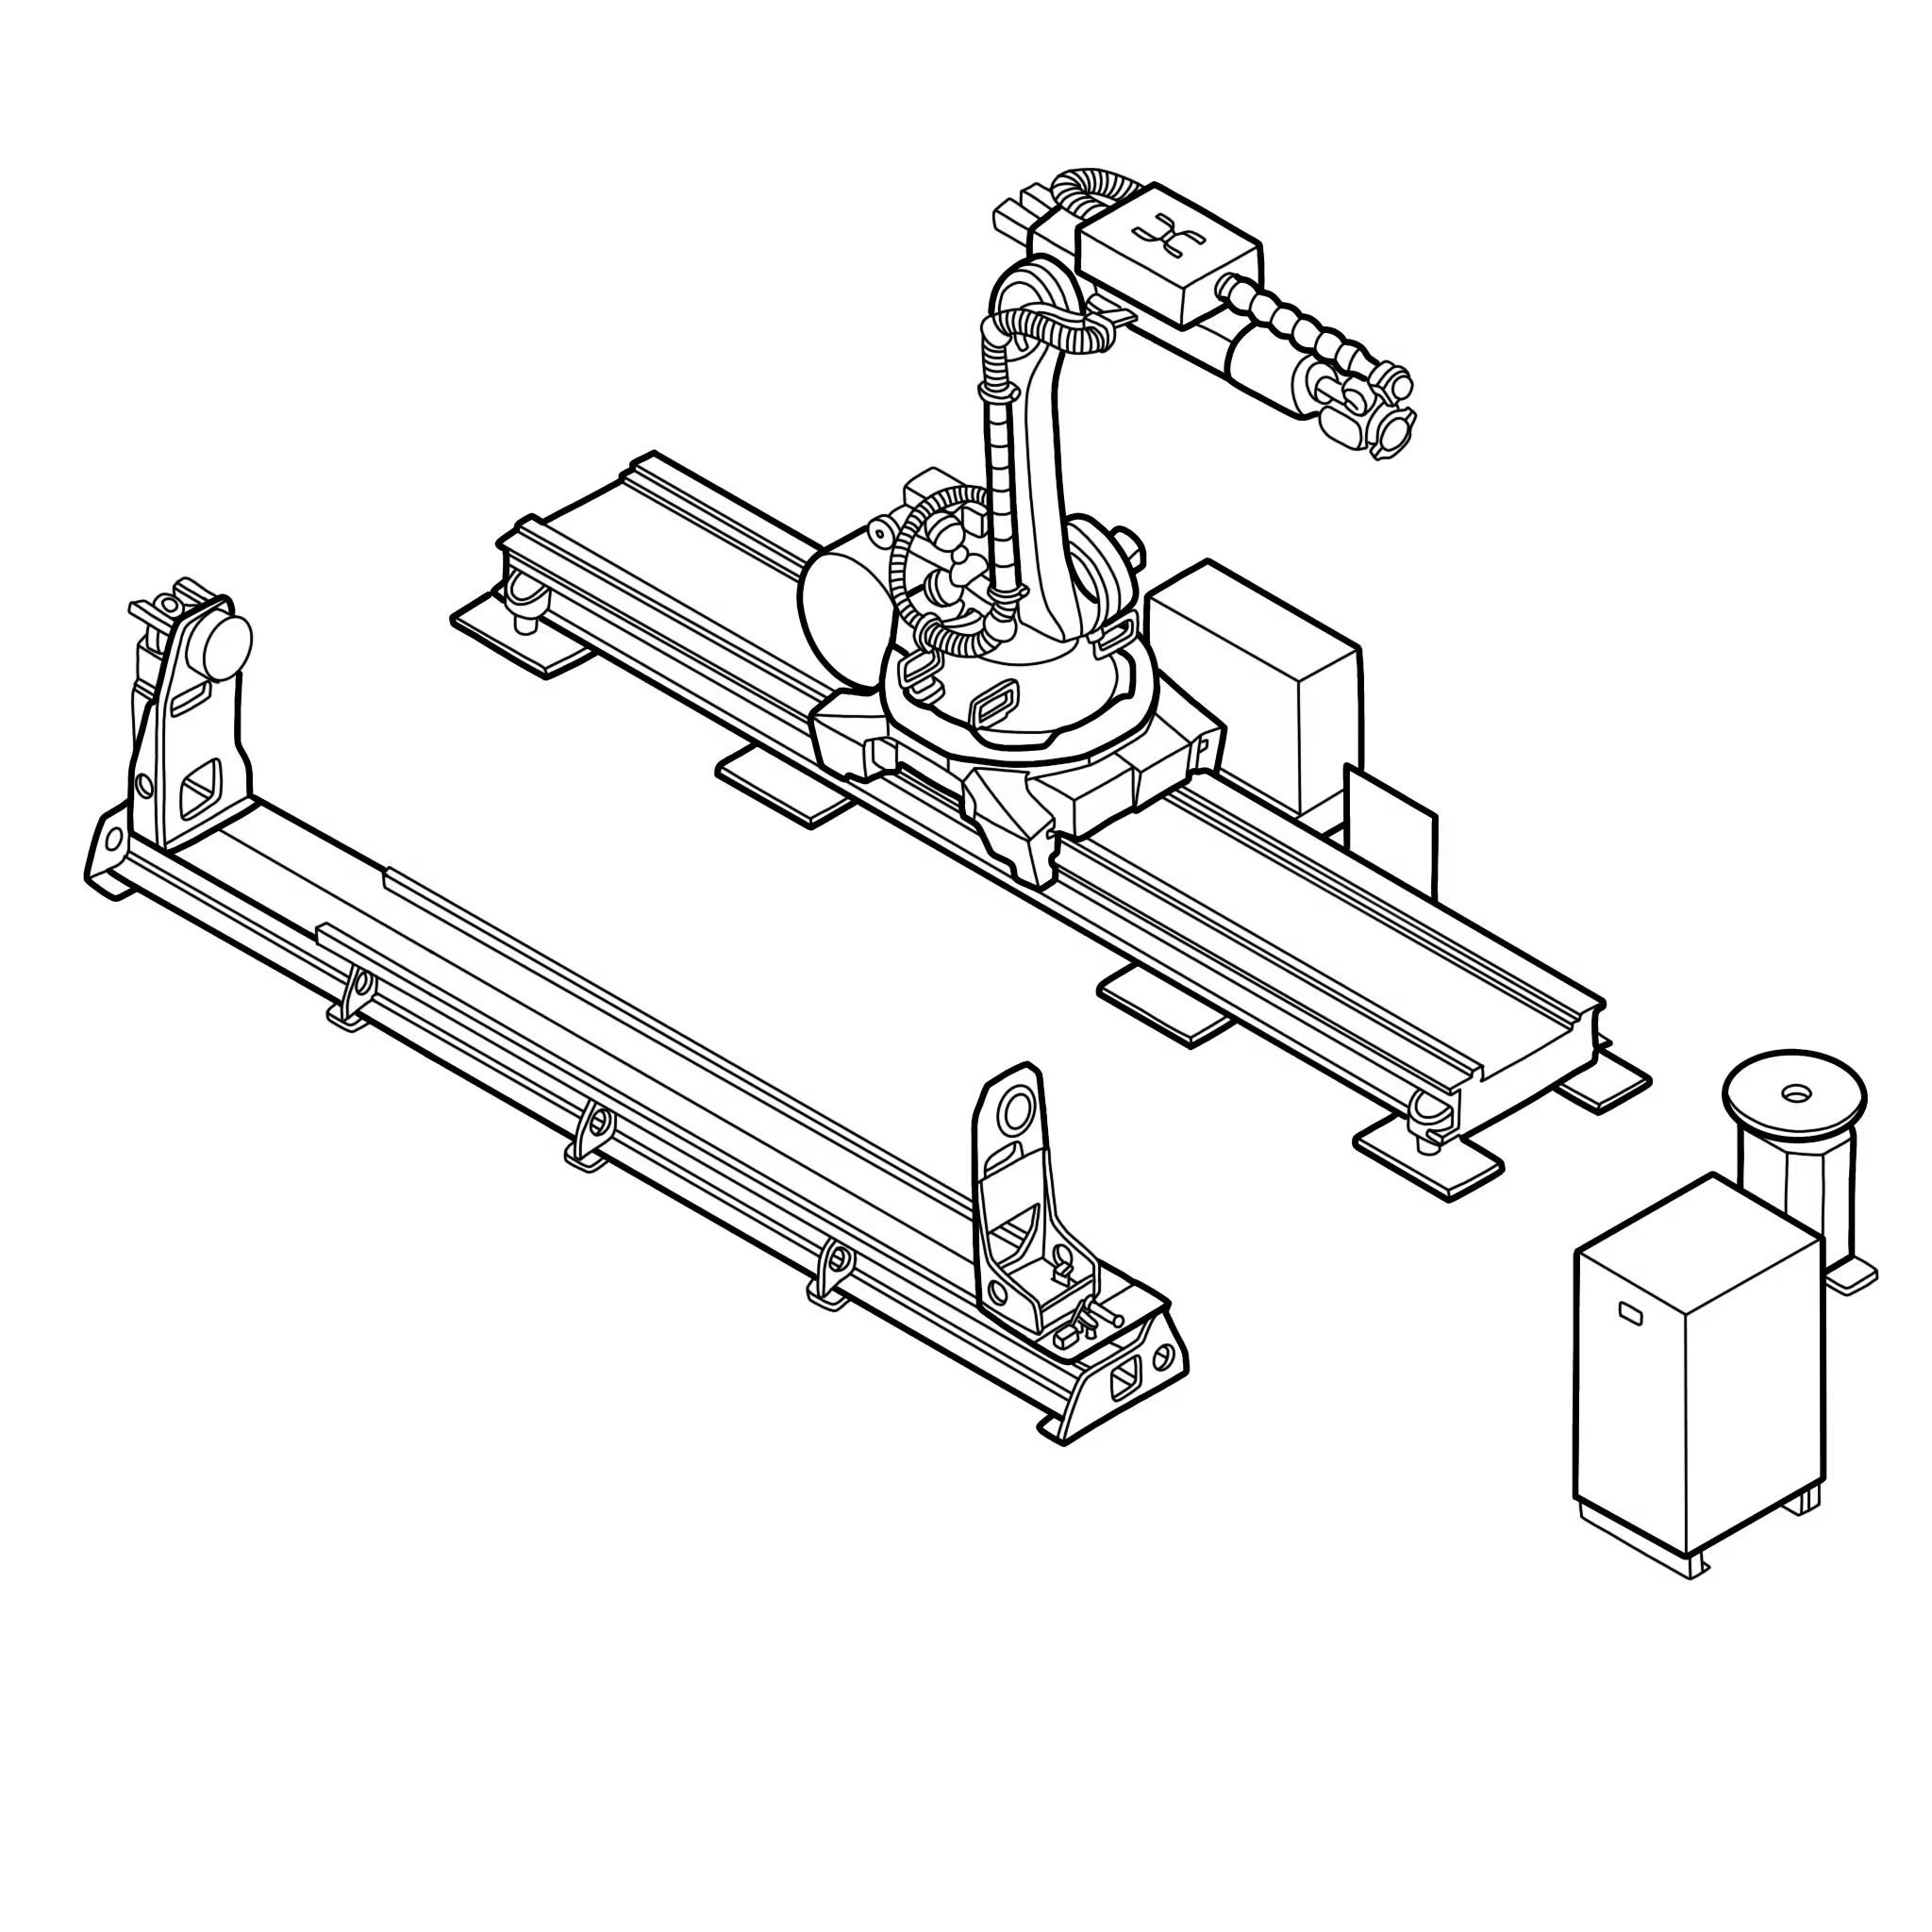
KUKA KR10-R1100-2, 6-axis robot
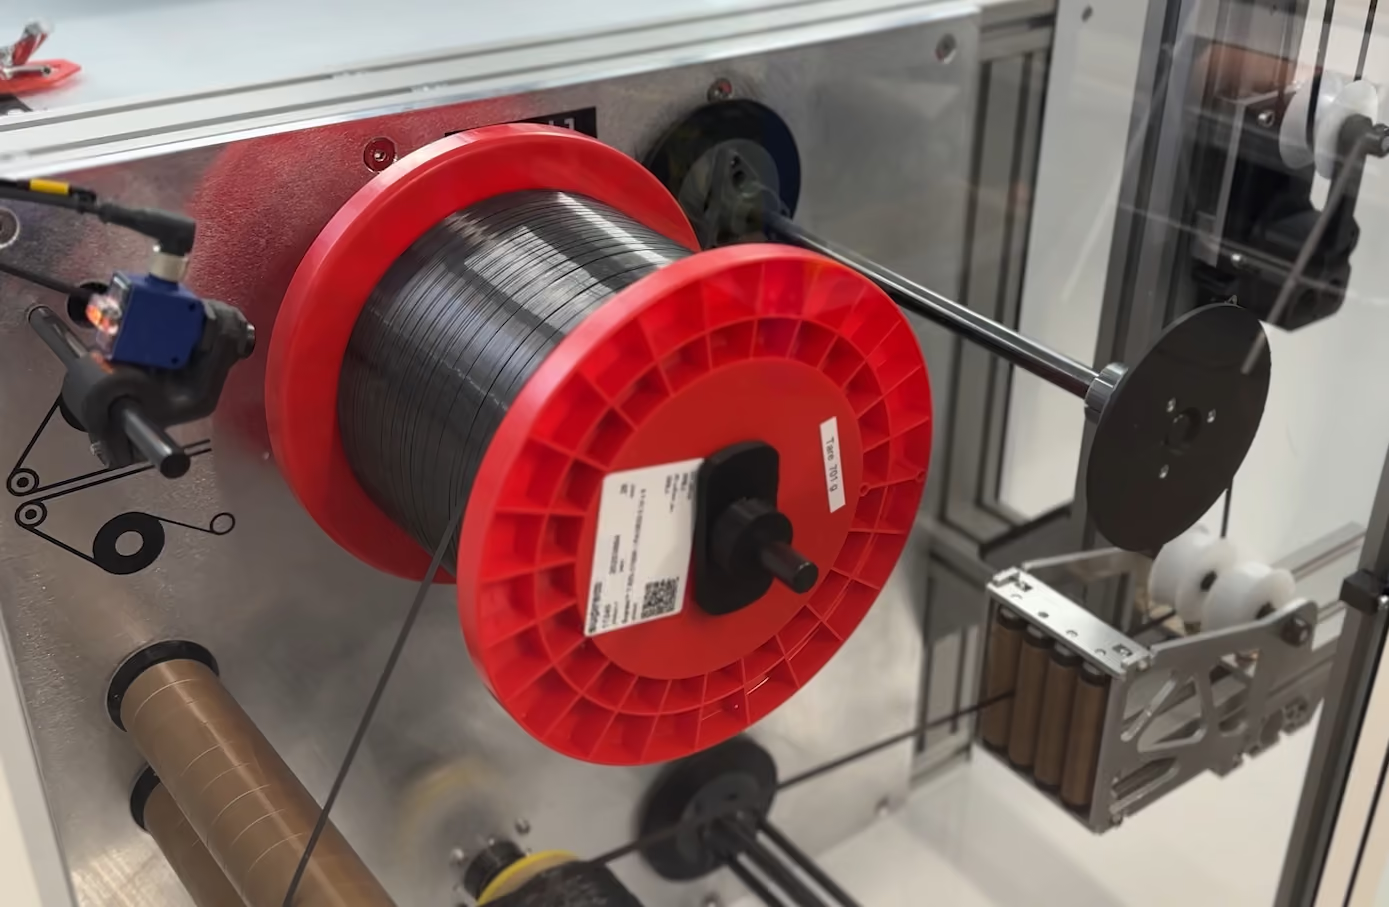
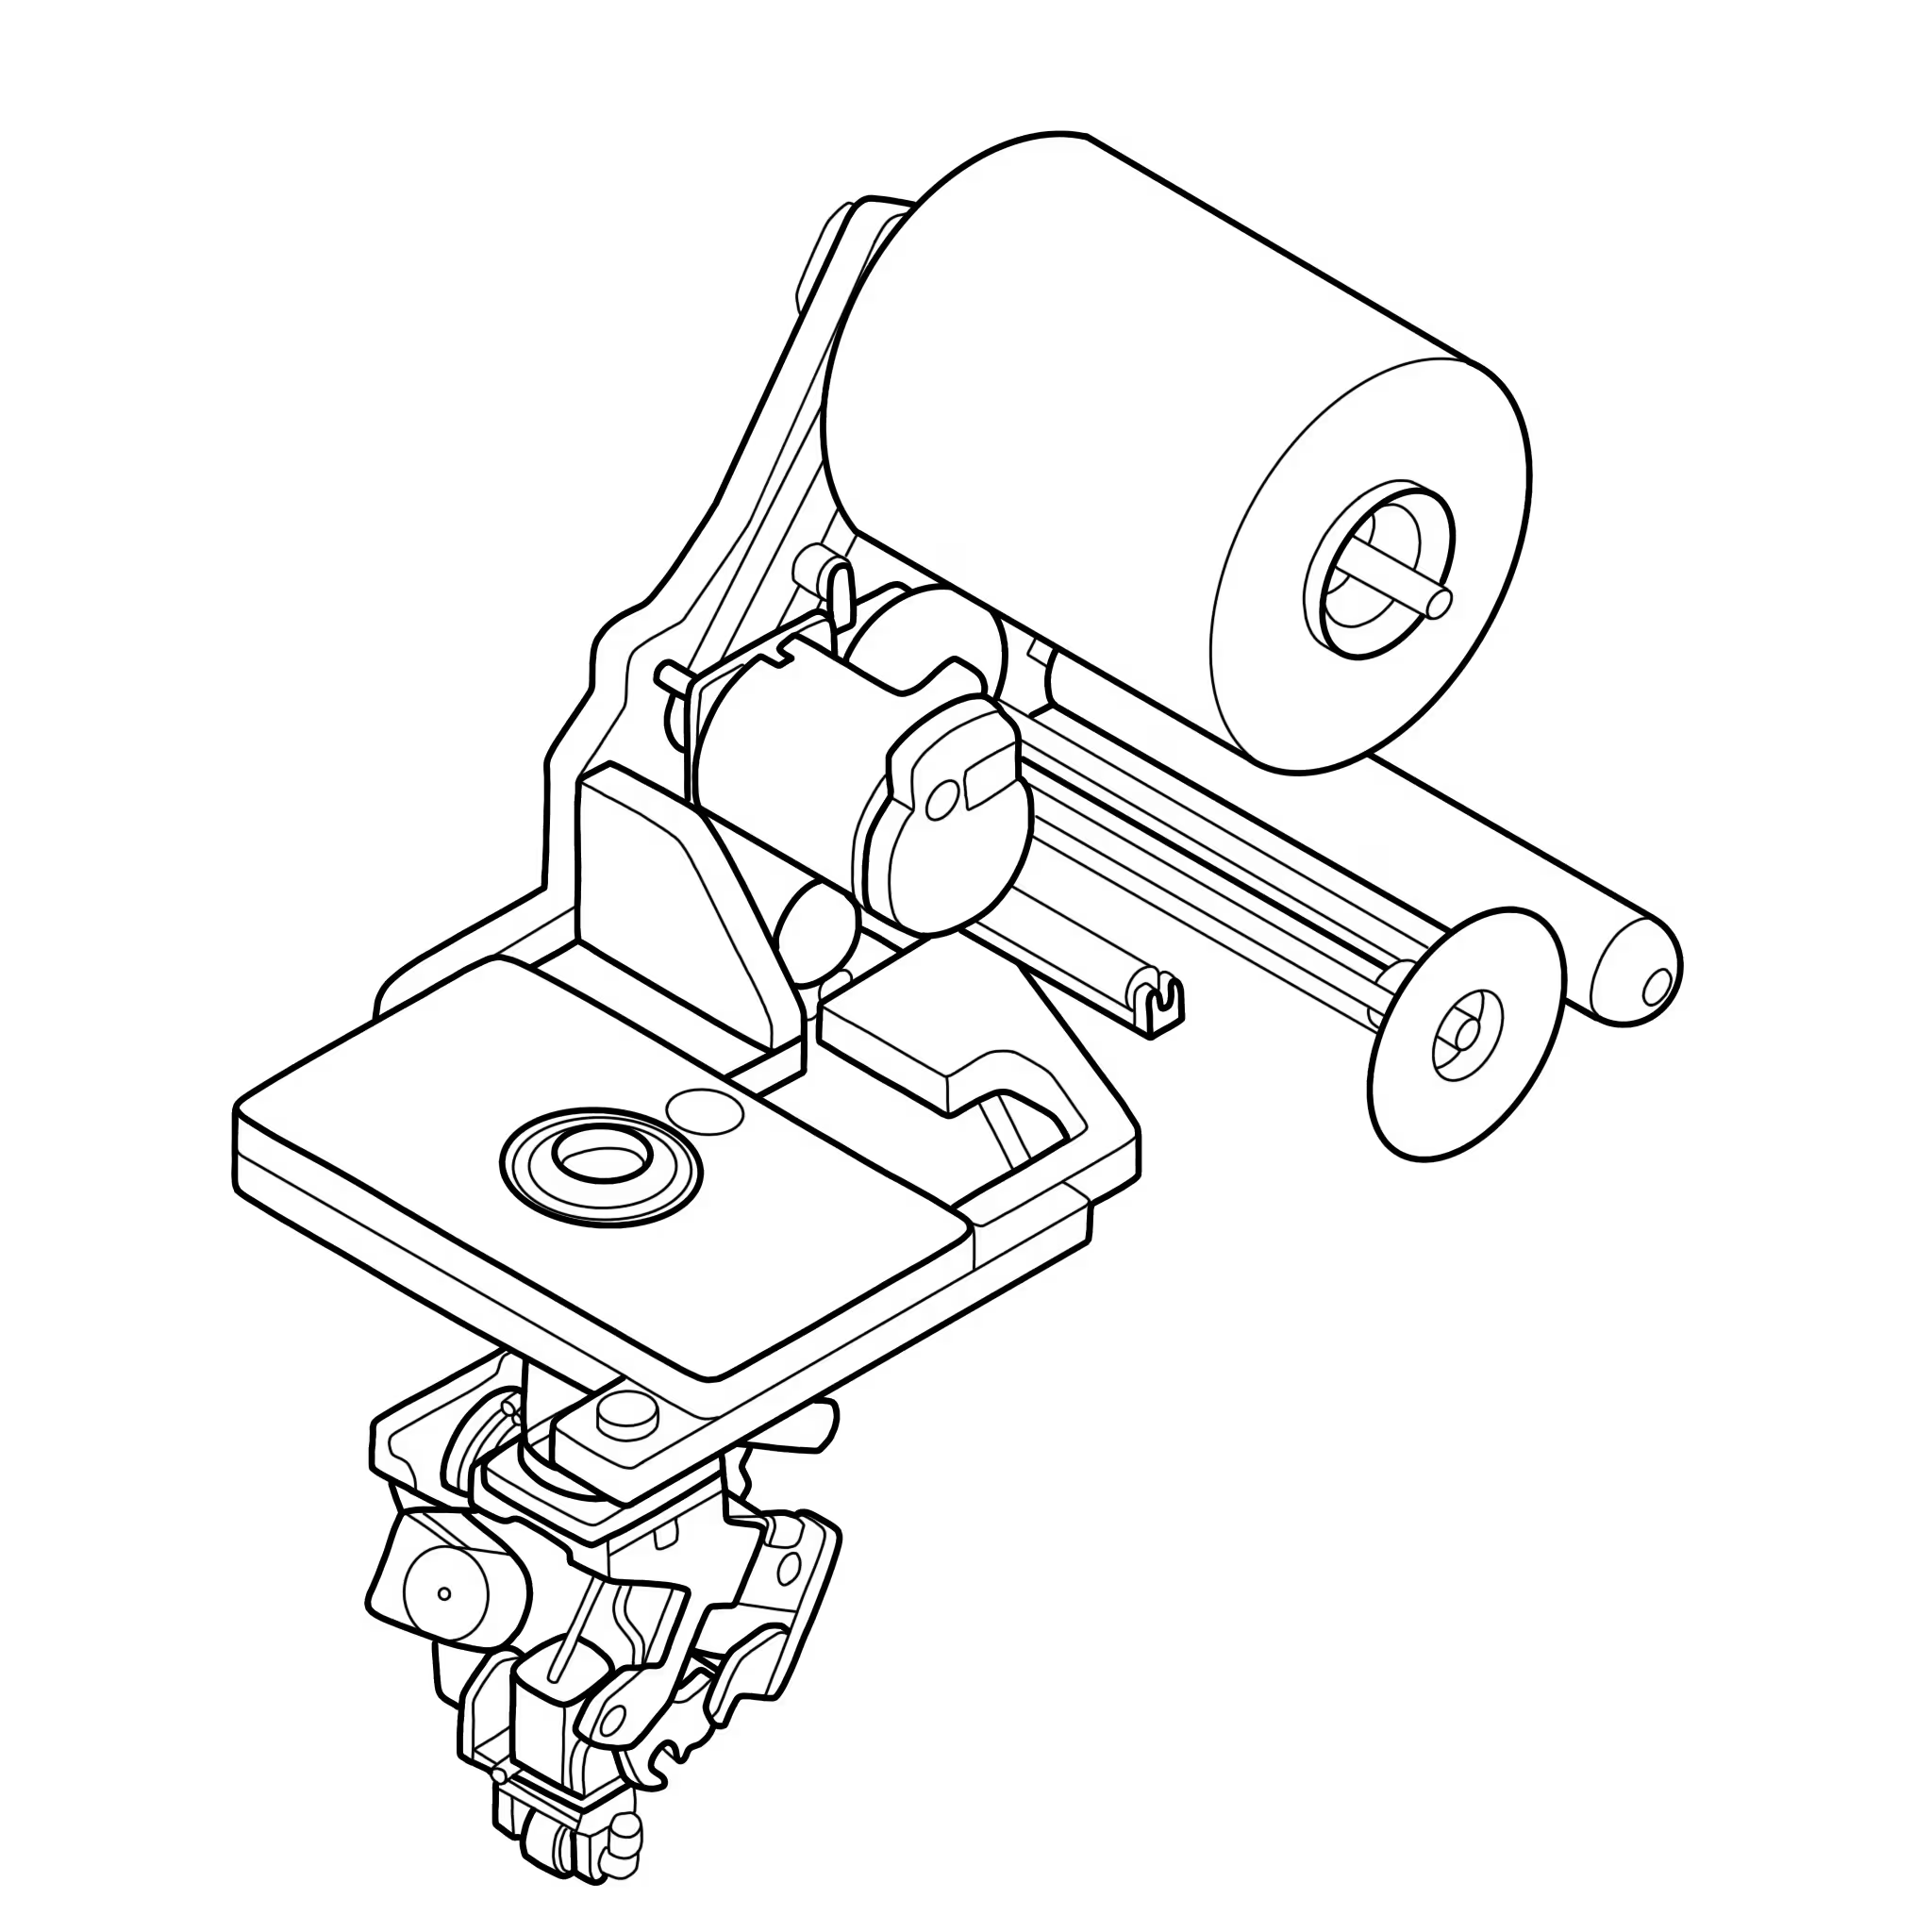
Fixed creel storage with tension control
Compatible spools: 3" cardboard core, Cassette BSH315 Hafner, and Hybrid DIN250 spools
Temperature-controlled enclosure
Power :230 V single-phase
KUKA KR10-R1100-2, 6-axis robot
Fixed creel storage with tension control
Compatible spools: 3" cardboard core, Cassette BSH315 Hafner, and Hybrid DIN250 spools
Part Size
Turn Table:
Max part size: L900 x W500 x H500 mm
Max mold/mandrel weight: approx. 50 kg
Horizontal positioner:
Max mandrel weight: 15kg
Max length between chucks: 900mm
Max mandrel diameter: Ø500mm
Max part size: L900 x W500 x H500 mm
Max mold/mandrel weight: approx. 50 kg
Horizontal positioner:
Max mandrel weight: 15kg
Max length between chucks: 900mm
Max mandrel diameter: Ø500mm
Layup Area
Turntable: Ø750mm
Horizontal positioner (optional): max 900mm between chucks
Horizontal positioner (optional): max 900mm between chucks
Processes
Automated Fibre Placement (XPlace mk3)
Filament Winding
Ultrasonic Cutting
3D printing
Filament Winding
Ultrasonic Cutting
3D printing
Connectivity
Siemens PLC
PROFINET and ETHERCAT
OPC UA server, live machine data
XPert Log: web app for live status and history
PROFINET and ETHERCAT
OPC UA server, live machine data
XPert Log: web app for live status and history